
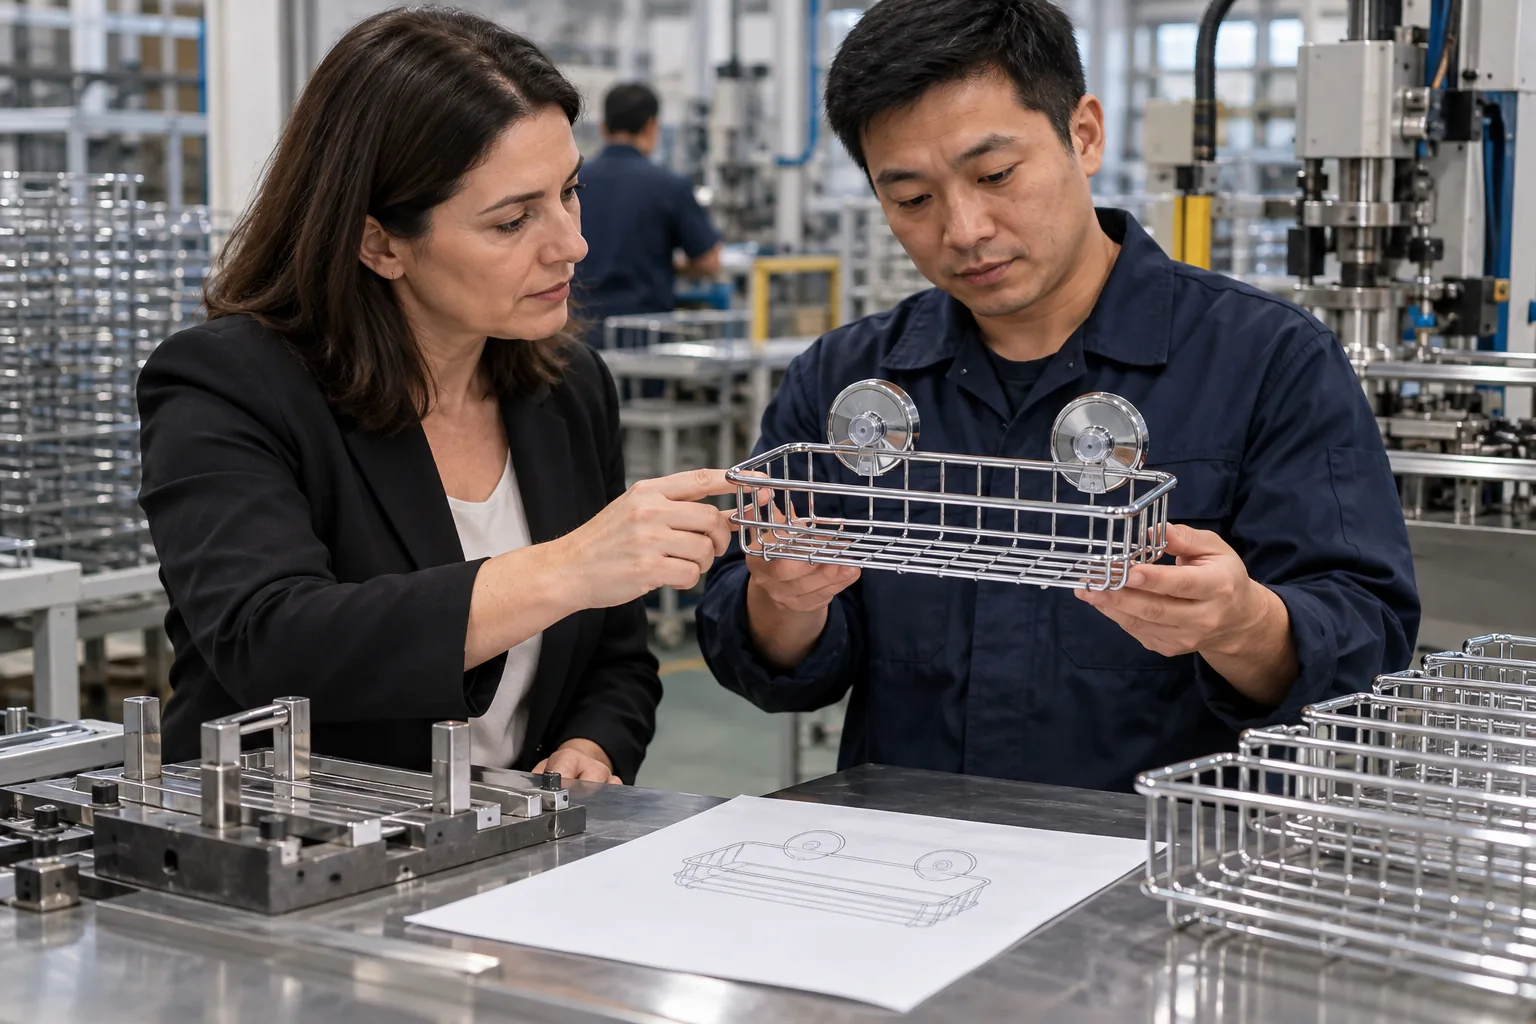
Supplier capacity takt time cycle time changeover are related planning concepts, but none alone proves that a hardware supplier can meet a buyer’s order plan. A buyer should connect the required shipment schedule to the actual product mix, demonstrated process route, available production time, quality losses, and setup changes. Ask for the assumptions behind a capacity statement and validate them on a representative product rather than treating a theoretical machine rate as committed output.
What do takt time and cycle time tell the buyer?
Takt time is a planning relationship between the time available for production and the customer demand to be served during that period. It indicates the pace a process would need to support under the stated assumptions. It is not the same as a proven production cycle, and it should not be presented as a supplier’s guaranteed output.
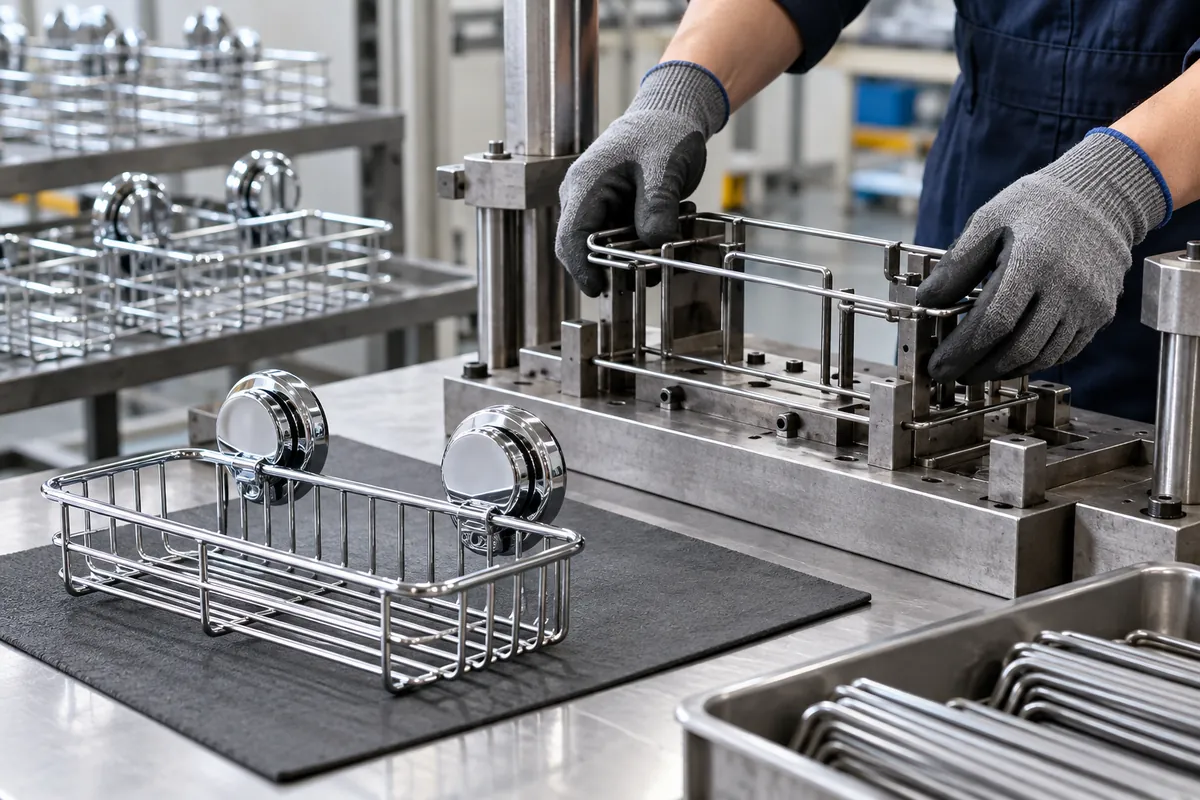
Cycle time describes the elapsed time associated with a defined process or operation. Its meaning depends on the boundary: one weld, one formed component, one assembled basket, or a completed packaged unit may all have different cycles. Ask the supplier which operation, product, and measurement window the stated time describes. A cycle measured on a stable single operation does not automatically include material handling, inspection, rework, replenishment, breaks, changeovers, or downstream bottlenecks.
When assessing supplier capacity takt time cycle time changeover, the buyer’s demand also needs definition. Forecasts may mix SKUs, finishes, pack configurations, and release dates. A monthly quantity divided by nominal calendar hours may not match the hours actually assigned to that product family. State the required mix and timing before comparing demand with a process rate. If mix is uncertain, request scenarios and label each assumption instead of converting a single projection into an unsupported commitment.
How do changeovers alter usable capacity?
A changeover is the planned work required to move a process from one product, size, material, finish, fixture, or setup to another. For wire and tube hardware, the work might involve a fixture change, tool adjustment, parameter confirmation, sample check, or line clearance, depending on the actual process. The scope differs by supplier and product. Do not assume a particular machine, workcell, or procedure exists without confirmation.
When product variety is high, repeated changeovers can consume a meaningful share of the time available for production. A quote based on an ideal steady run may omit those transitions. Ask how the supplier’s estimate treats setup, first-piece checks, adjustment, cleaning, and approval between batches. If several product variants share a process, request the assumptions for the proposed sequence and lot sizes.
Changeover time is not automatically waste; some setup is necessary to preserve correct geometry, finish, or assembly. The buyer should not pressure a supplier to omit verification steps merely to improve a quoted rate. Instead, understand which activities are included, which are excluded, and what evidence confirms the new setup is ready. A sample or first-piece approval may be required after certain changes, subject to the buyer’s control plan.
What should a buyer ask when a supplier states monthly capacity?
First clarify whether the number refers to a single operation, a complete finished product, or a family of items. Ask whether it describes theoretical maximum, recent demonstrated output, available capacity after other orders, or a commercial commitment. Those are different statements. A supplier may have a fast process step but limited downstream polishing, coating, assembly, inspection, or packing capacity; buyers should ask which stage controls the stated result.
Request the assumptions that make the estimate meaningful: product and revision, material/finish, order size, SKU mix, routing, working calendar, planned shifts if applicable, setup frequency, downtime allowance, quality disposition, and packing configuration. Some suppliers may share a summary rather than confidential line-by-line schedules. The buyer needs enough evidence to assess the plan, not another customer’s private details or unrestricted access to factory records.
Compare the required demand with the process evidence over a defined period. A historical shipment total without a time window or SKU context is hard to interpret. A sample run can demonstrate a route under specific conditions but does not establish repeatable monthly output. A planning model can be useful if it states inputs and uncertainty. Keep measured observations, supplier estimates, and commitments clearly separated in the sourcing record.
| Capacity evidence | What it can support | Buyer limitation or follow-up |
|---|---|---|
| Theoretical cycle estimate | A first-pass process-rate calculation for a defined operation | Does not include the full route, losses, mix, or schedule availability |
| Representative sample run | Evidence that a specific route produced a defined sample under observed conditions | Does not prove repeatability or capacity across other SKUs |
| Historical output summary | Context about prior output when product mix and time window are known | May not represent current available capacity or future demand |
| Supplier capacity plan | A forecast under documented work-calendar and process assumptions | Confirm bottlenecks, setups, quality losses, and other order commitments |
| Purchase-order delivery commitment | Commercial responsibility for the agreed quantity and date | Must be backed by agreed scope, milestones, change handling, and communication |
Do not use one evidence type to imply another. A documented sample run is not a guarantee; a capacity plan is not an independent audit; and a purchase-order commitment is not a technical measurement. The buyer can request different evidence for different decisions.
How can a buyer check the full manufacturing route?
For supplier capacity takt time cycle time changeover review, map the major operations from material or purchased input through forming, joining, finishing, assembly, inspection, and packaging as applicable to the proposed product. The route should be project-specific; a bathroom basket and a sheet-metal shelf may use different operations. The purpose is not to collect a generic factory tour but to identify where the schedule can queue and which supplier or process owns each step.
Ask which steps are performed by the quoted supplier and which rely on approved subcontractors or purchased parts. Outsourced processing can be a normal part of a supply chain, but it changes coordination, transport, traceability, and available-time assumptions. Do not assume that coating, plating, molding, or a specialist test is performed in-house. Record the stated source and approval route if relevant.
Look for bottlenecks rather than adding nominal operation rates together. If a process feeds slower finishing or inspection, the fastest step does not define complete-product capacity. Ask how work-in-process is scheduled and what evidence supports the stated handoff times. Avoid requesting confidential customer information; anonymized or product-family summaries may be sufficient for a buyer review.
Quality performance affects usable output too. A gross quantity may include pieces awaiting inspection, rework, or disposition. Ask whether the estimate is good units ready for packing or total units started. Define how scrap, rework, first-piece approval, and hold stock are treated. If no reliable historical data is available, label it as unknown and use a controlled pilot or staged order rather than manufacturing a precision percentage.
What should go into a sourcing or launch plan?
For a new program, separate development milestones from repeat-production capacity. Drawing review, material confirmation, tooling or fixture readiness, sample fabrication, finish approval, packaging review, and production release are not interchangeable with the steady-state cycle. Agree on what must be approved before a production order is scheduled and who can authorize a deviation.
For repeat orders, document expected release windows, SKU mix, quantity, and required ship date. Ask the supplier to identify planning assumptions and any known constraints early. If demand changes, use a clear revision or order-change process so both parties can reassess setup, material availability, outsourced steps, and pack-out. Do not assume a previous capacity estimate still applies after a product, mix, source, finish, or schedule change.
A buyer’s evaluation should protect both delivery and quality. Staging orders or using a pilot can reveal whether the route, inspection plan, packaging process, and communications work as expected. This does not replace supplier qualification or a contract, but it makes assumptions visible. For smaller OEM runs, flexibility may be more valuable than a headline maximum rate; compare the actual commercial need, not an abstract factory-size claim.
Buyer checklist
– Define the exact product family, revision, finish, SKU mix, quantity, and required timing.
– Ask whether stated capacity is theoretical, demonstrated, available, planned, or committed.
– Identify the operation and product boundary behind every cycle-time figure.
– Separate operating time from setup, inspection, changeover, adjustment, and planned downtime assumptions.
– Map the proposed route and identify bottleneck or outsourced steps.
– Clarify whether output means units started, accepted, packed, or ready to ship.
– Request sample or historical evidence tied to the relevant product and time window.
– State what information may be summarized to protect other customer confidentiality.
– Document assumptions, uncertainty, open questions, and the owner of each follow-up.
– Reassess the plan when product, mix, finish, source, tooling, or delivery schedule changes.
What should trigger capacity revalidation?
Revisit the estimate when the product design or revision changes; a new finish, material, or supplier source is proposed; the SKU mix or lot size shifts; a fixture or process route changes; production is moved to another facility; a new inspection or packaging requirement is added; or the buyer requests a materially different schedule. These are prompts to reassess the assumptions, not a claim that every change requires the same formal audit.
Record the previous estimate and identify which inputs changed. Ask the supplier whether the change affects cycle, setup, yield, outsourced lead time, or final pack-out. If the evidence is incomplete, use a staged confirmation—such as revised sample approval or a limited production run—before relying on the old plan for a larger release. Make the decision proportionate to business risk and available evidence.
Keep supplier conversations factual and collaborative. A mismatch between a forecast and actual output may arise from changed demand, setup frequency, material availability, quality holds, or route constraints. Separate the observed shortfall from its cause. A corrective plan should state actions, owners, and dates without inventing capacity metrics or attributing blame unsupported by records.
Frequently asked questions
Is takt time the same as machine cycle time?
No. Takt time relates available production time to customer demand under stated assumptions. Cycle time describes a process or operation interval. A buyer should compare them only after defining the process boundary, demand period, product mix, and included losses.
Can a sample run prove monthly capacity?
It can show that a specific sample route ran under observed conditions. It does not by itself prove sustained output across multiple orders, variants, shifts, or constrained downstream processes. Ask what additional evidence supports the planning horizon.
Should the buyer request the supplier’s complete production schedule?
Not necessarily. The buyer can ask for product-relevant assumptions, a capacity summary, milestone status, and early warning of constraints without demanding confidential records for other customers. Agree on a useful evidence format.
Do changeovers always reduce output?
They use time, but they may be essential to make the next product correctly and safely. Understand what setup and verification activities are included rather than asking a supplier to remove controls to improve a headline rate.
How should buyers compare two supplier capacity claims?
Use the same product, process boundary, time period, SKU mix, quality basis, and order scenario. Mark which values are estimates versus observed data and ask each supplier to explain exclusions. A bare monthly figure is not a comparable metric.
What if a supplier cannot provide reliable historical capacity data?
Keep the limitation explicit. Consider a controlled sample or pilot order, milestone reviews, and a delivery plan that reflects uncertainty. Do not replace missing records with an invented production-rate assumption.
Discuss a product-specific sourcing plan
Share the product drawing or sample, finish, SKU mix, target order schedule, and required pack-out so a supplier discussion can focus on the actual route and assumptions. Koitor is a specialized OEM manufacturer of bathroom and home-storage hardware; project-specific capacity and timing should be confirmed rather than inferred from generic claims.
Discuss your OEM production requirements
Share the product definition, order mix, and target schedule for a project-specific sourcing discussion.
OEM / PRIVATE LABEL
Turn this sourcing guide into a product brief
Share your target product, size, finish, order quantity and packaging requirements. Your team receives a practical manufacturability review before quotation.
 English
 Español
 Português
 Français
 Deutsch
 العربية