

Lot split merge genealogy outsourced finishing traceability is the buyer’s way to answer a practical question: when a hardware order is divided among finishing batches, moved between suppliers, combined for packing, or returned for rework, can the buyer still connect each shipped carton to the relevant production and finishing records? A lot number on one traveler is not enough if the identity disappears at a handoff. The buyer and supplier should agree how incoming parts, each outsourced process batch, exceptions, and final packed quantities remain linked.
This matters for metal bathroom and home-storage hardware because the product may pass through forming, welding, polishing or coating, inspection, assembly, and packaging. Some processes may be performed by a specialist supplier. This article offers a buyer-control framework, not a claim about Koitor’s current subcontractor network or the traceability system of any specific factory. The level of identification should match the project’s risk, volume, customer requirements, and the records each party can actually maintain.
Why can an outsourced finishing handoff break lot identity?
The risk often appears during an ordinary operational change. A factory releases one production lot to a finishing provider, but the batch is divided across two racks or process runs. Some pieces are held for appearance review. A small portion is reworked. Another portion is sent back for a second pass. Later, accepted pieces may be packed together to fill an order. Each action can be reasonable, but a buyer needs to know whether the resulting records preserve the path from source lot to finishing batch to final shipment.
If the identity is lost, the buyer may not be able to answer which order, product revision, process run, or cartons are involved when a question arises. That does not automatically mean the product is defective. It means the available evidence may be too coarse to isolate what should be reviewed. Conversely, extensive individual serialization may create unnecessary marking and data work for a product whose agreed risk control is batch-level. The buyer should select a proportionate method with suppliers before shipment, not after an issue appears.
GS1’s Global Traceability Standard describes traceability across objects and parties, including transformation, aggregation, and disaggregation events, and notes that batch/lot identification is one possible level. That framework is a useful reference for thinking about handoffs, but it does not impose a specific internal record format on every bathroom-hardware order. Buyers should not claim GS1 conformity unless their parties have implemented the applicable requirements and evidence supports that statement.
What should the buyer define before the first finishing shipment?
Begin with the order and product identity. The finishing provider should be able to identify what it received: buyer or supplier part number, drawing revision, finish specification, source lot, quantity, date, and sender. The record must distinguish products that look similar but have different revisions or finish requirements. If the buyer has a lot convention, state who assigns it and whether each partner must preserve it or map it to a local identifier.
Next define the process event. A finishing lot may be a specific run, rack load, batch, or other grouping according to the provider’s actual operations. The supplier should explain what the identifier represents rather than applying the word “lot” without a consistent definition. When one source lot is divided, each child batch should retain a link to the parent. If multiple source lots are combined in a run, the record should list each contributing parent and the quantities, subject to the supplier’s practical control method. If a combined output cannot be segregated reliably, the buyer needs to know before approving that arrangement.
The buyer should specify, at minimum, how these transitions are recorded:
- Receipt by the finishing provider, including source identity, quantity, and date.
- Any split into separate loads, runs, or inspection groups, with a parent-to-child mapping.
- Any merge or combination, showing every contributing lot and its quantity.
- Hold, rejection, rework, strip-and-refinish, or other exception status.
- Final acceptance and return quantity, including scrap or unexplained variance.
- Repacking or aggregation into cartons and shipment units.
- Record retention, access, and the person responsible for updating each event.
These are buyer control points, not mandatory fields in every industry standard. The contract, quality agreement, customer requirements, and supplier capability determine the final record. The core outcome is that a buyer can follow the material through the specific operations and identify which finished quantity belongs to which approved source and process conditions.
How should split, merge, and rework events be documented?
A split should create traceable child identities or another controlled mapping. For example, if a supplier sends a production lot to a finisher and the work is separated into distinct process runs, each run can have an identifier that points back to the original lot. The exact format may be a traveler, barcode, ERP record, or controlled spreadsheet; the buyer should evaluate the reliability of the method, not select a technology for appearance alone. Labels should remain readable and attached to the physical container or rack during movement, while the record remains recoverable if a label is damaged.
A merge should preserve every input. If accepted parts from multiple source lots enter a shared finishing run, the resulting record needs to retain those inputs rather than assigning a new code that erases them. If the operation creates a new combined group, that new identifier should point backward to the contributing lots and forward to the returned or packed quantities. A one-to-many or many-to-one relationship is the important concept; the article does not prescribe a data standard or software implementation.
Rework needs its own status and event link. Do not quietly relabel a rejected or stripped group as if it were untouched production. Record what was held, why it was held at the level permitted by the project’s quality process, what action was authorized, what quantity was reprocessed, and how the outcome was accepted. Keep the original process history; adding a new event should not overwrite the prior state. A buyer may not need a detailed defect narrative for every low-risk order, but the amount and kind of information must be agreed, available, and suitable for the project’s obligations.
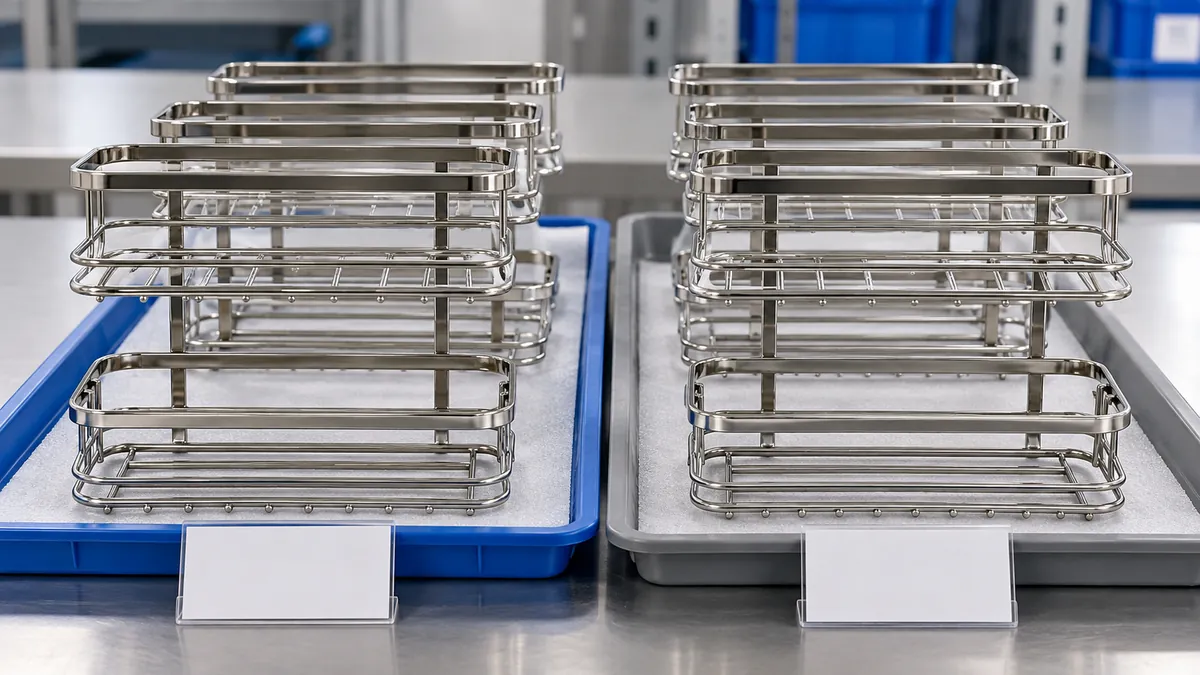
When the finishing provider returns goods, reconcile the quantity sent with accepted, held, reworked, scrapped, and returned quantities. Do not invent a yield percentage or treat every difference as a defect. Instead, define how the supplier explains variance and who must approve disposition. If cartons are repacked or combined, preserve a mapping between package IDs and their contents at the level the buyer needs. This prevents a logistics-unit label from becoming a substitute for product-lot history.
Which traceability approaches should buyers compare?
The appropriate approach depends on how much isolation the buyer needs and what suppliers can sustain. The table compares practical options; it is a decision aid, not a prescribed GS1 implementation.
| Approach | What it can support | Buyer evidence to request | القيد الرئيسي |
|---|---|---|---|
| One lot identity carried through each handoff | Basic batch-level link from incoming parts to returned finished goods | Receipt, process, inspection, and shipment records using the same controlled identity | Breaks down when one lot is split, merged, or repacked without a mapping |
| Parent-child batch genealogy | Connects one source lot to multiple process runs or combined outputs | Split/merge event record showing parent IDs, child IDs, quantities, dates, and status | Requires disciplined updates at each transfer; a spreadsheet can still be unreliable if ownership is unclear |
| Container or rack identification plus transaction log | Helps maintain physical segregation during movement | Label format, scan or sign-off event, reconciliation, and exception process | A label alone does not prove the record is accurate or that contents were not mixed |
| Item-level serialization | Can identify individual units where the project requires that granularity | Agreed serial assignment, capture points, and records linking units to process events | Adds marking, capture, and data-management effort that may be disproportionate for some hardware orders |
GS1 references batch/lot and instance-level identification as distinct options whose suitability depends on the traceability objectives and supply chain. That principle is useful for buyers: choose the minimum granularity that can answer the real questions. Do not ask for serial-level records simply because a system can produce them, and do not accept a single order-level label if several materially different finishing runs need to remain distinguishable.
What should supplier evidence look like at sample and production stages?
At supplier qualification or sample stage, walk through a representative handoff using the proposed record format. Ask the supplier to show how it creates the incoming identity, applies a finishing-run identity, records a split or hold, and maps accepted goods to the return. The exercise should use a real project sample or a clearly identified demonstration. A conceptual example is not proof that production operators follow the same controls.
For production, request records tied to the purchase order and part revision. Depending on the agreement, these may include a dispatch list, receiving acknowledgment, process-run or rack-load reference, inspection disposition, rework authorization, return note, and final carton mapping. The buyer should not demand confidential records beyond the agreed scope; it should confirm that relevant evidence can be retrieved if a quality or delivery question occurs.
Review consistency, not decorative formatting. Do the lot IDs match between documents? Are quantities reconciled? Is the record dated and attributable to a responsible party? Can the supplier explain gaps, corrections, or replaced labels? Are held and reworked goods physically separated from accepted stock? Where a process provider uses its own identifier, is a cross-reference maintained? These checks expose whether genealogy survives normal production activity.

Photographs can document physical segregation or visible labels, but they cannot by themselves prove a complete genealogy. A blank or unreadable card in an illustrative image is not a real record. For production approval, review actual controlled documentation or a live demonstration within the supplier relationship. Avoid publishing customer names, order identifiers, proprietary process details, or personal information from a real traceability record.
How should buyers write traceability into an RFQ or quality agreement?
State the business question the traceability control must answer. Examples include identifying which process batch supplied an order, isolating finished goods affected by a specific finishing run, or confirming what happened to material held for rework. Then define the granularity, event points, fields, record owner, format, retention period, and response expectation. These requirements should be realistic for the order size and supplier chain.
For lot split merge genealogy outsourced finishing traceability, buyers should explicitly ask what happens when a production lot is divided among several finishing runs, when different lots share a run, and when material is returned for rework. Require the supplier to preserve the source-to-output relationships and reconcile quantities. If the provider’s internal system assigns its own run code, require a cross-reference to the buyer’s or supplier’s original lot identity. Decide whether the buyer needs to approve a merge across product revisions or only receive notification. A lot split merge genealogy outsourced finishing traceability plan should name who owns each parent-child link and which production record demonstrates the final count.
Make change control part of the agreement. A change in finishing provider, facility, process route, identification method, record retention, or carton consolidation could affect the agreed evidence chain. Ask suppliers to notify the buyer when a change may invalidate prior sample evidence or prevent the required lot mapping. The buyer should define when renewed approval is needed rather than assume that every process change has the same effect.
Keep the requirement concise enough to operate. A small trial order may need a simple controlled dispatch/return record with explicit split mapping. A more complex program may need structured electronic events or a customer-specific format. The supplier should state what it can provide, and unresolved gaps should be handled before the order is released. Do not promise real-time visibility, automatic recall capability, or a certification unless the responsible supplier can demonstrate it.
Buyer checklist and frequently asked questions
Before approving the traceability plan, confirm:
- The incoming part number, drawing revision, source lot, finish requirement, and quantities are identified.
- Every split creates a controlled mapping to the parent lot.
- Every merge lists contributing lots and resulting quantities.
- Holds, scrap, rework, and repeat finishing retain a visible history and disposition.
- Returned finished quantities reconcile with sent and processed quantities.
- Repacking or carton consolidation does not erase required lot relationships.
- Each record has an owner, date, status, and agreed retention period.
- The supplier has demonstrated the method on a sample or representative transaction.
- Supplier and facility changes trigger the defined review or notification path.
Does a lot number prove full traceability?
No. A lot code is an identifier, but buyers also need records that connect relevant events, parties, quantities, and transformations. If a lot is divided or combined, the relationship must be retained in a mapping or event record.
Should buyers require serial numbers for every basket or bracket?
Not by default. Individual serials may be appropriate when project risk, customer rules, or regulatory requirements call for instance-level control. Many sourcing decisions can use an agreed batch-level method. Select the granularity based on the question the buyer needs to answer and the supplier’s demonstrated process.
Can a finishing provider use its own batch code?
Yes, if the buyer’s required relationship is preserved. The provider’s code should be cross-referenced to the original source lot and the returned quantity. The parties should agree who maintains the mapping and how it is retrieved.
What if two lots are combined in one finishing run?
The record should identify the contributing lots and the combined process group, then preserve the link to the returned or packed output. If the buyer needs to keep those sources physically separate, specify that instead of assuming segregation.
Is a photograph of labelled bins enough evidence?
It can support a visual review, but a photo does not demonstrate that identifiers match shipment documents or remain linked through later rework and packing. Review the underlying transaction record or a representative trace exercise.
Does a traceability framework certify a supplier?
No. A published framework can provide concepts and common language. Supplier conformity, certification, and system effectiveness require specific evidence and should not be inferred from a general reference.
Source
Discuss Supplier Traceability Requirements
Share the hardware drawing, finishing handoff, or traceability question for an OEM project. Koitor can discuss the manufacturing and sourcing requirements within the confirmed project scope; actual supplier records and capabilities must be verified for the specific order.
OEM / العلامة التجارية الخاصة
حوّل دليل التوريد هذا إلى موجز منتج
يرجى إطلاعنا على المنتج المستهدف، والحجم، والتشطيب، وكمية الطلب، ومتطلبات التغليف. وسيتلقى فريقك تقييمًا عمليًّا لإمكانية التصنيع قبل تقديم عرض الأسعار.


 English
 Español
 Português
 Français
 Deutsch
 العربية