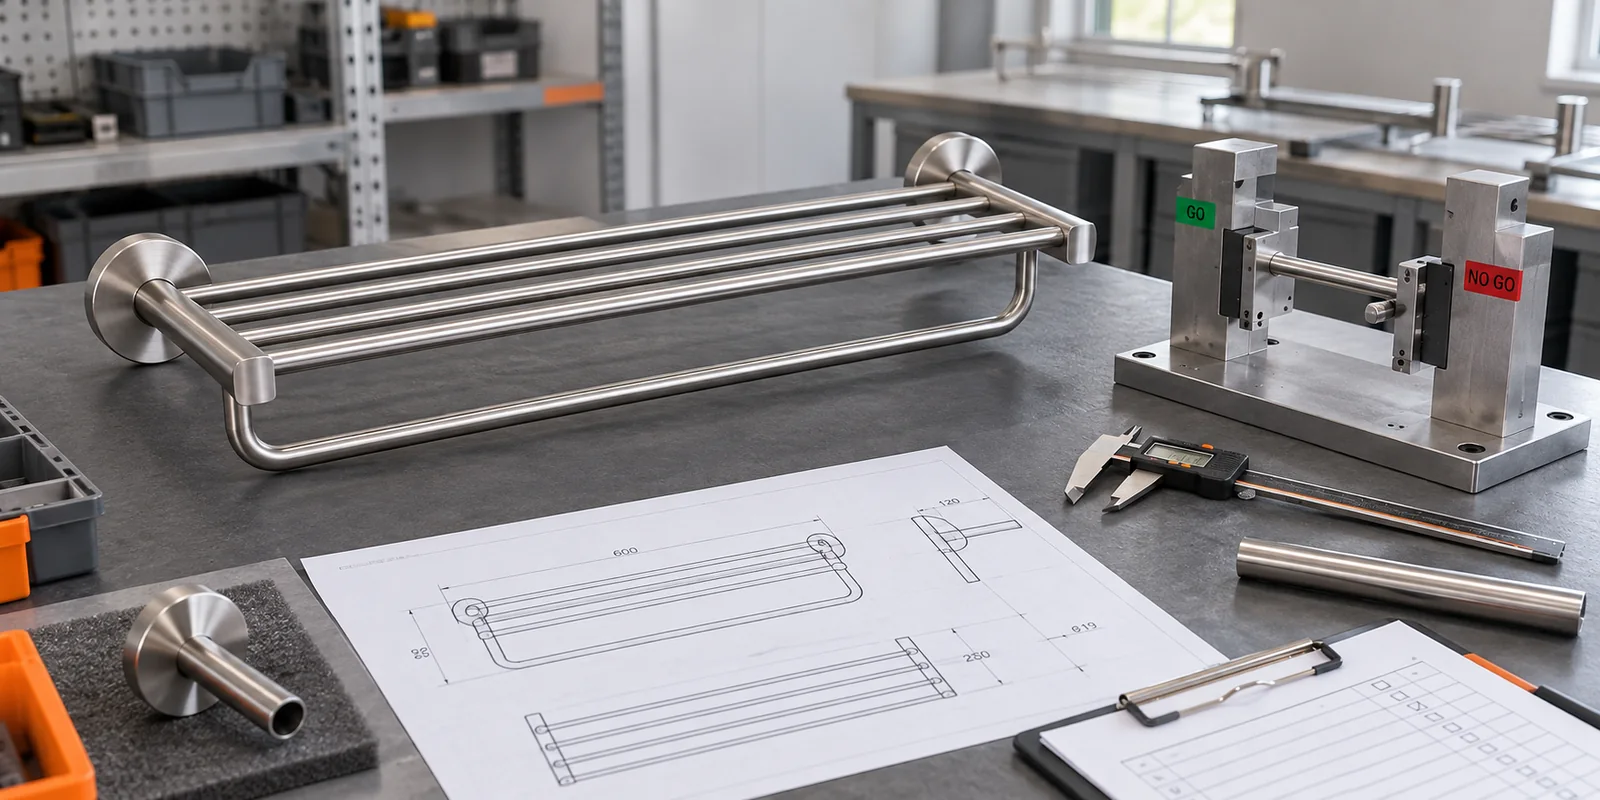
Bathroom hardware inspection gauge design should be approved as part of the complete product and packing system, not treated as a minor detail after production starts. For towel racks, tissue holders, wire baskets and other repeat bathroom hardware programs, buyers should define function, measurement references, sample checks, acceptance points and record ownership before comparing quotations. A clear specification reduces interpretation gaps while still giving the manufacturer room to recommend a practical production method.
What Does Bathroom Hardware Inspection Gauge Design Mean for Buyers?
In practical OEM sourcing, bathroom hardware inspection gauge design means the design of a checking fixture or template that compares a finished part with approved dimensional limits without requiring a full measurement routine each time. The decision affects product appearance, production consistency, inspection, packing and repeat orders. It should therefore appear in the drawing, packing specification or quality plan that both buyer and supplier use.
The first buyer task is to define the product context. State where the product will be used, which surfaces or interfaces matter, how the item is assembled or installed, and which dimensions or cosmetic zones are critical. A supplier cannot make a reliable recommendation from a product name alone. Representative photos are helpful, but dimensioned drawings, approved samples and written acceptance language carry more control.
Separate functional requirements from preferences. A functional requirement affects fit, stability, handling, protection, assembly or identification. A preference affects visual direction but may allow more than one manufacturing solution. Labeling the two groups helps Koitor Hardware discuss alternatives without accidentally changing a critical buyer requirement.
Buyers should also define the approval unit. It may be one finished sample, a paired component set, a packed retail unit or a complete master carton. The right approval unit reflects the point where the feature can genuinely be evaluated. Reviewing an isolated component may miss interactions that appear after finishing, assembly or packing.
Koitor Hardware is a family-owned custom metal hardware factory supporting flexible small-batch OEM work from buyer drawings or physical samples. The Fertigung von maßgefertigten Badbeschlägen page provides a useful starting point for discussing this type of product, while the Koitor sourcing resources page connects related buyer guidance.
Which Design or Control Options Should OEM Buyers Compare?
Buyers should compare options against the intended product, finish, assembly route, order quantity and inspection method. A lower-cost detail is not economical when it creates packing damage, confusing assembly, unstable fit or repeated sorting. Likewise, the most complex option is not automatically the best when a simpler controlled solution meets the requirement.
| Option | Suitable use | Main advantage | Main buyer check |
|---|---|---|---|
| Go/no-go gap gauge | Repeated clearances and openings | Fast pass-or-recheck decision | Define which finished surfaces may contact the gauge |
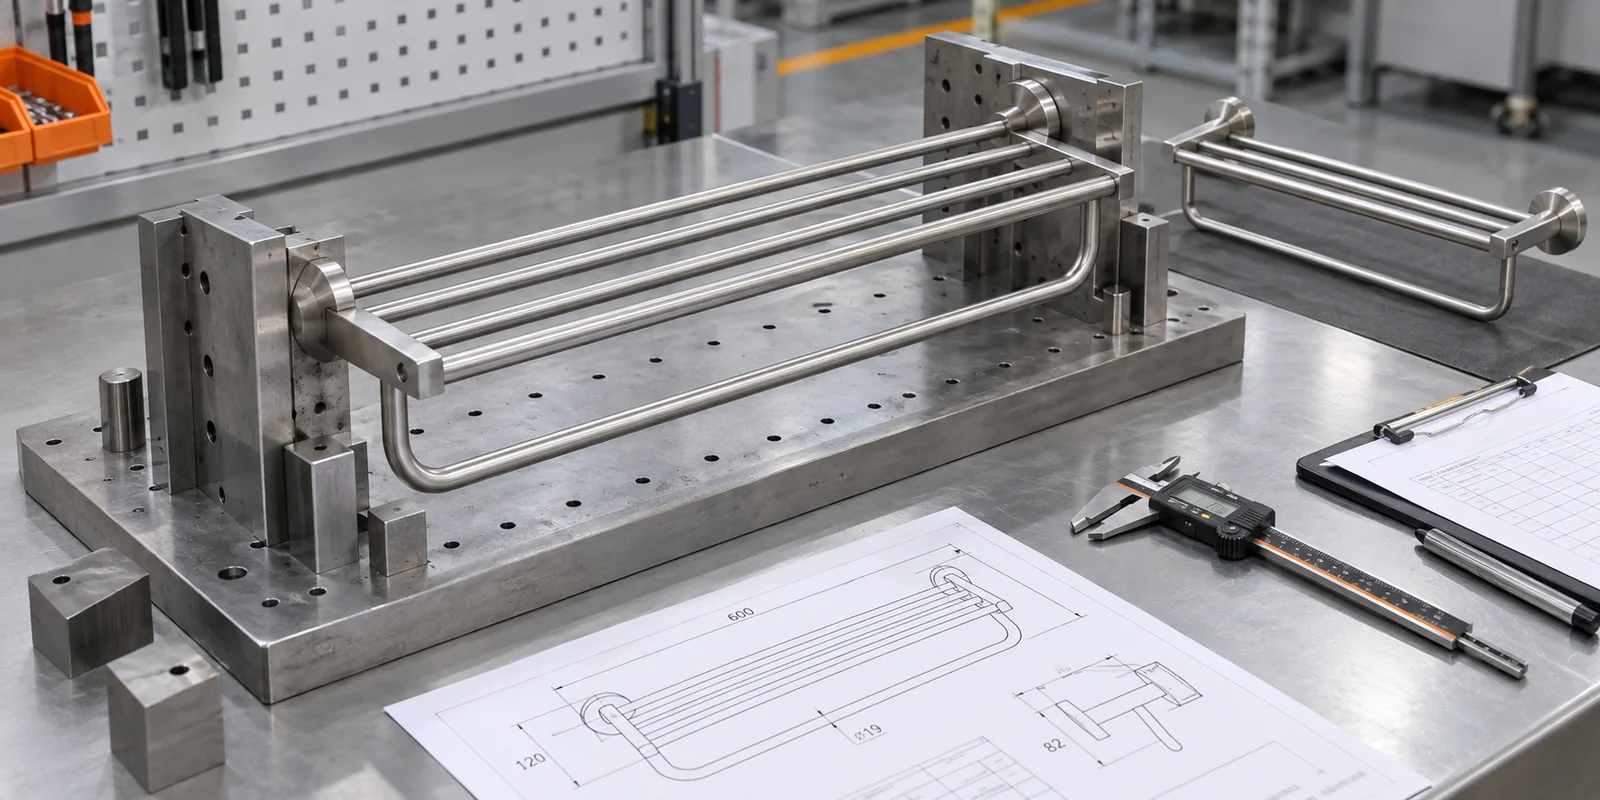
| Hole-spacing fixture | Two-bracket wall products | Checks mounting centers together | Use a stable datum and allow the intended slot direction |
| Profile or contour template | Bent wire and formed frames | Makes shape drift visible | Control the template edge and viewing direction |
| Flatness and squareness board | Frames, shelves and racks | Shows twist and corner relationship | Specify support points and permitted rocking |
| Approved master-sample comparison | Complex visual assemblies | Combines appearance and geometry review | Protect, identify and periodically verify the master |
Use the table as a discussion guide rather than a universal ranking. Ask the supplier to state what is included in the quotation and which assumptions affect tooling, fixtures, components, labor or packaging. Two prices are not comparable when suppliers have interpreted the detail differently.
For a trial order, favor an option that can be inspected clearly and repeated without excessive manual judgment. Small-batch production still needs controlled references. A flexible factory can adjust fixtures, parts and packing methods, but repeated undocumented adjustments make later orders harder to match.
The approved option should be identified by a drawing revision, sample label or specification revision. Avoid relying on email photographs alone because cropping, lighting and scale can hide important differences. When an alternative is proposed, record why it is being considered and which downstream checks must be repeated.
What Should the Specification and Drawing Include?
The specification should tell the production and inspection teams what to make, where to measure and how to judge the result. It does not need unnecessary technical language, but it must remove ambiguity around critical buyer expectations. For bathroom hardware inspection gauge design, include these items:
- inspection characteristic and drawing reference.
- product datum and loading orientation.
- go and no-go limits where applicable.
- gauge contact points and protected cosmetic zones.
- fixture material and wear surface.
- operator sequence and decision rule.
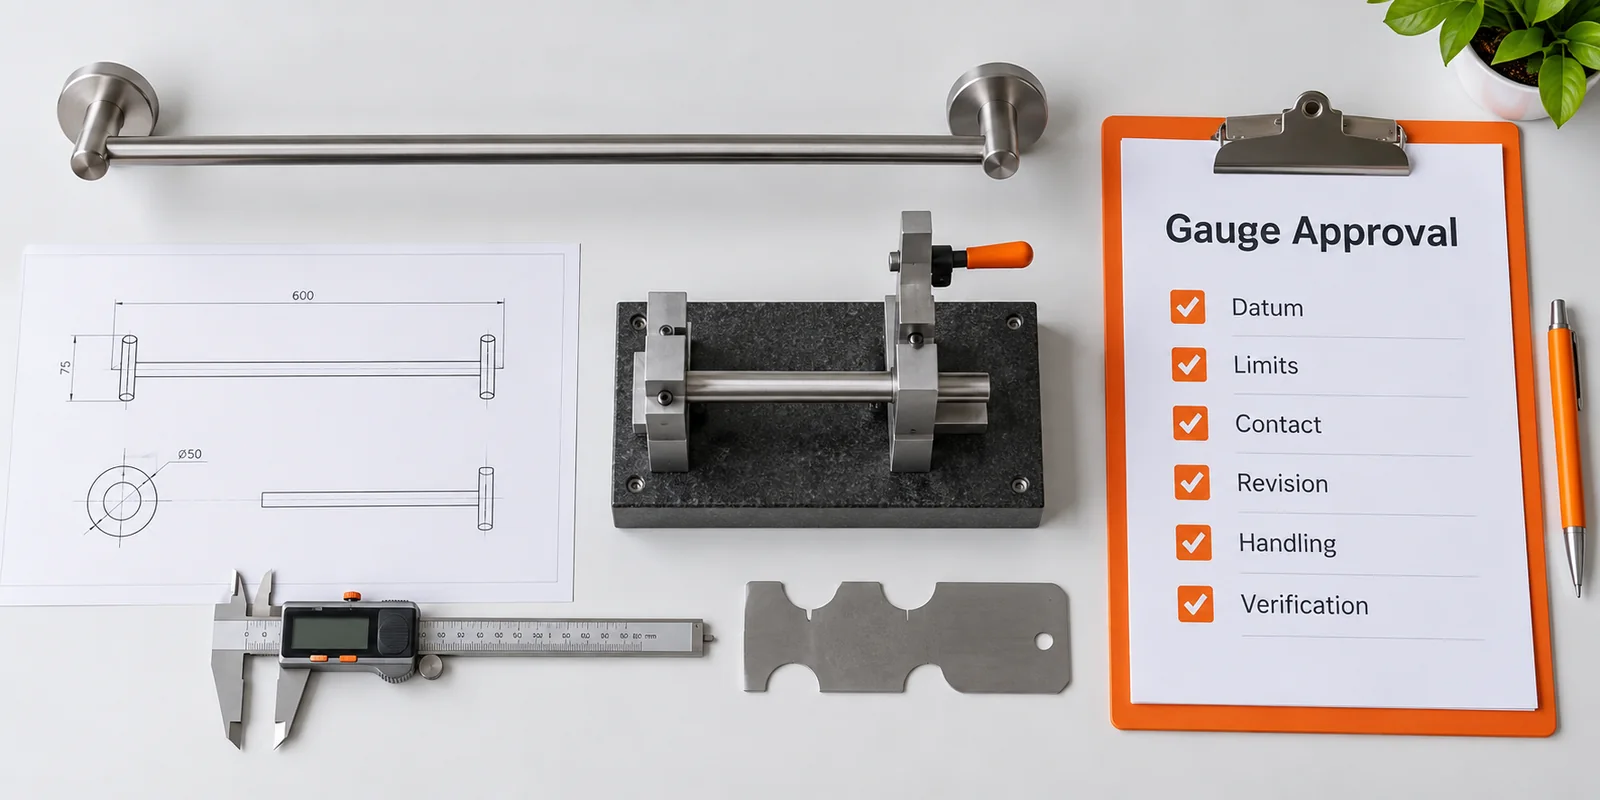
- gauge identification and revision.
- verification interval and master reference.
Add references that make measurements reproducible. Identify datum surfaces, product orientation and whether dimensions apply before or after finishing. If a physical sample controls appearance, label it with the project, revision and approval date. If a drawing controls geometry, ensure the sample and drawing do not contradict each other.
Tolerance should follow function. Tight tolerances on every feature can increase checking and production difficulty without improving the product. Mark critical fit, assembly and cosmetic points separately from reference dimensions. Ask how the proposed process naturally varies, then choose acceptance limits that protect the buyer’s application.
The specification should also explain what happens after a change. A revision to material, finish, packaging, mating component or installation method can affect the feature even when its own drawing value appears unchanged. Use controlled revision notes and reapprove the relevant checks rather than assuming an earlier result still applies.
Important requirements should remain in server-readable article text, drawings and purchase documents, not only in an image or chat message. This improves internal retrieval and helps sourcing, quality and logistics teams work from the same information.
How Should Samples and Production Trials Be Approved?
Sample approval should recreate the real interfaces that can change the result. Use the intended material, finish, components, packing materials and assembly sequence whenever possible. A prototype made from substitute parts can answer an early geometry question, but it should not become the final production reference without clear limitations.
- Rank product characteristics by fit, installation and repeat-production risk.
- Choose only stable dimensions that benefit from rapid fixture checking.
- Define the same datum used on the controlled product drawing.
- Build a gauge and test it with accepted and deliberately varied samples.
- Check that normal operator force cannot change the decision.
- Record the inspection sequence with photographs and clear acceptance language.
- Approve the product sample, drawing and gauge revision as one control set.
Keep observations factual. Record the sample condition, method, result and reviewer instead of writing only “approved.” Photographs should show the full product and close details with a measurement reference where useful. Do not use photographs as a substitute for recording dimensions or acceptance criteria.
Koitor can review a drawing or sample and discuss a practical manufacturing route, but the buyer should confirm market-specific requirements for the destination and use. Product claims, loading statements or compliance statements need project evidence; they should not be inferred from appearance or a generic sample.
Once approved, protect the reference from uncontrolled changes. Store the latest file in a known location, identify the master sample, and retire superseded versions. Repeat orders should cite the same controlled revision unless a change has been formally approved.
Which Production Variables Need Ongoing Control?
Production control should focus on variables that can change fit, appearance, handling, packing or traceability. The factory and buyer should agree which checks happen at incoming material, forming, welding, finishing, assembly, packing and final inspection. Not every characteristic needs inspection at every stage, but each critical result needs a responsible checkpoint.
- Product location against the datum: record the agreed requirement, sample observation and inspection method.
- Gauge wear or edge damage: record the agreed requirement, sample observation and inspection method.
- Coating thickness at contact points: record the agreed requirement, sample observation and inspection method.
- Operator force and viewing angle: record the agreed requirement, sample observation and inspection method.
- Weld distortion after assembly: record the agreed requirement, sample observation and inspection method.
- Revision mismatch between drawing and fixture: record the agreed requirement, sample observation and inspection method.
For bathroom hardware inspection gauge design, first-piece review is especially useful. A first piece or first assembled set can reveal fixture setup, material substitution, component mismatch or packaging interference before the complete batch progresses. The record should identify what was checked and whether production was released.
Sampling frequency should reflect process risk and order structure. A mixed-SKU order, new component, revised tool or new finish may need more attention than an unchanged repeat order. The buyer can request a practical control plan without dictating every factory operation. Clear outputs matter more than a long checklist copied from another product.
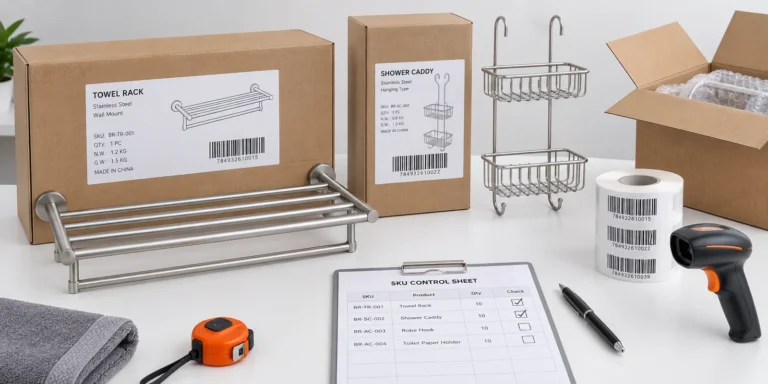
Final inspection should confirm the agreed feature on finished, packed-condition products. Where packing hides the detail, inspect before closure and retain a record that connects the result to the final lot. Visible carton or unit identification should match the purchase and packing documents.
Buyers evaluating broader capabilities should prepare drawings, samples and order assumptions before discussing the project with the factory. This allows the first review to focus on product decisions instead of reconstructing missing background.
What Buyer Checklist Prevents Common Sourcing Mistakes?
A useful checklist connects commercial, technical, quality and packaging decisions. Complete it before quotation, repeat it at sample approval and review changed items before repeat production.
- ☐ Confirm the exact product, SKU and intended use.
- ☐ Identify the controlled drawing and sample revision.
- ☐ Mark critical dimensions, interfaces and cosmetic zones.
- ☐ State material and finish assumptions without unsupported claims.
- ☐ Define the selected option and acceptable alternative process.
- ☐ Agree on sample quantity, approval evidence and responsible reviewer.
- ☐ Confirm assembly, installation and user-contact checks.
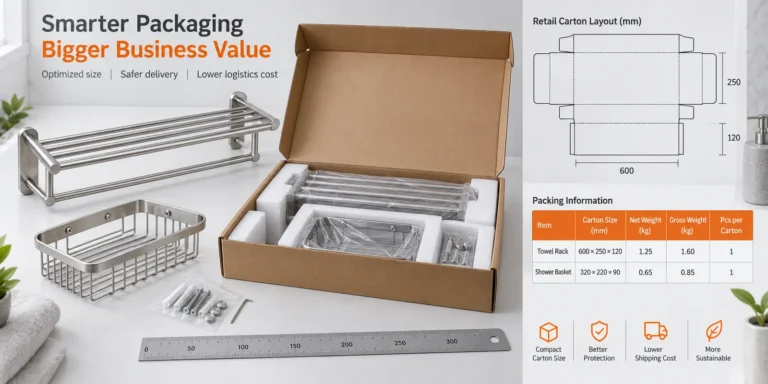
- ☐ Review retail pack, inner pack and master-carton interactions.
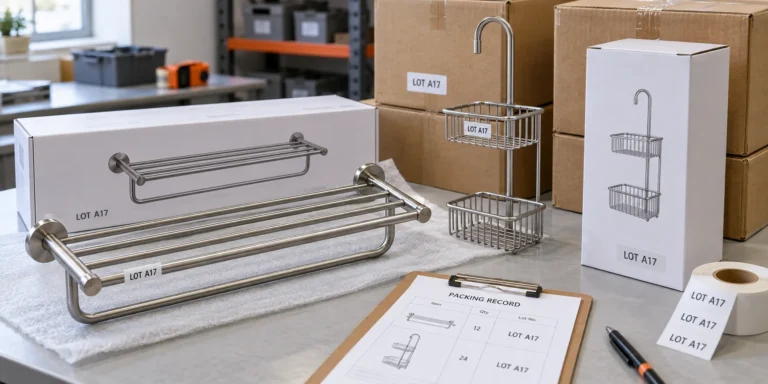
- ☐ Define lot identification and record references.
- ☐ Record changes before approving repeat production.
Common problems often begin with an incomplete handoff rather than an obviously poor manufacturing step. Watch for these mistakes:
- Avoid turning every drawing dimension into a separate custom gauge.
- Avoid using a flexible fixture that bends around a nonconforming part.
- Avoid placing gauge contact on a sensitive cosmetic finish.
- Avoid checking hole distance without defining the datum or slot direction.
- Avoid keeping an unidentified master sample beside current production.
- Avoid treating a quick fixture check as a replacement for all inspection records.
Before placing an order, ask the supplier to summarize open questions. This simple step exposes assumptions that may not appear in a quotation. Resolve the questions in one controlled specification, then reference that document in the purchase order.
For repeat orders, compare the new order against the last approved configuration. Confirm whether material, finish, dimensions, components, artwork, labels, inserts or carton quantities changed. Even a small change can require a focused sample check.
Prepare a short handoff pack for every approved SKU. It should contain the latest drawing, clear sample photographs, a list of critical features, the packing layout, label artwork, component list and open issue record. Name files consistently and show the revision on every controlled page. The sourcing manager, factory contact and inspector should be able to identify the same approved version without searching through separate message histories. When a decision changes, update the relevant file and record who approved it. This disciplined handoff is particularly valuable for small-batch OEM orders because development, purchasing and packing decisions can happen close together. It also makes future quotations more accurate: the factory can distinguish a true repeat order from a revised product that requires new samples, fixtures, components or packaging checks.
Häufig gestellte Fragen
When is an inspection gauge useful for bathroom hardware?
A gauge is useful when a critical dimension repeats frequently and a quick comparative check is more practical than measuring every feature with general instruments.
Does a go/no-go gauge replace a drawing?
No. The controlled drawing remains the dimensional authority, while the fixture helps operators apply selected limits consistently.
Which features should buyers prioritize?
Prioritize mounting centers, product profiles, clearances and assembly relationships that affect installation or fit with mating parts.
Can a finished coated part be placed in the gauge?
Yes when the fixture is designed for the finished condition and its contact areas will not mark the approved surface.
How should the fixture be approved?
Compare it with the controlled drawing, approved samples and known boundary samples, then record its identification and checking method.
How often should a gauge be verified?
Set an interval based on use, material and wear risk, and recheck it whenever damage, repair or a product revision occurs.
Arbeiten Sie mit Koitor Hardware zusammen
Need Help Planning Inspection Gauges for Bathroom Hardware?
Send Koitor your product drawing, approved sample and critical installation dimensions. The team can review practical fixture concepts and small-batch inspection checkpoints before quotation.
OEM / EIGENE MARKE
Verwandeln Sie diesen Beschaffungsleitfaden in ein Produktdossier
Teilen Sie uns Ihr Zielprodukt, die Größe, die Oberflächenausführung, die Bestellmenge und Ihre Verpackungsanforderungen mit. Ihr Team erhält vor der Angebotserstellung eine praxisorientierte Prüfung der Herstellbarkeit.
 English
 Español
 Português
 Français
 Deutsch
 العربية