
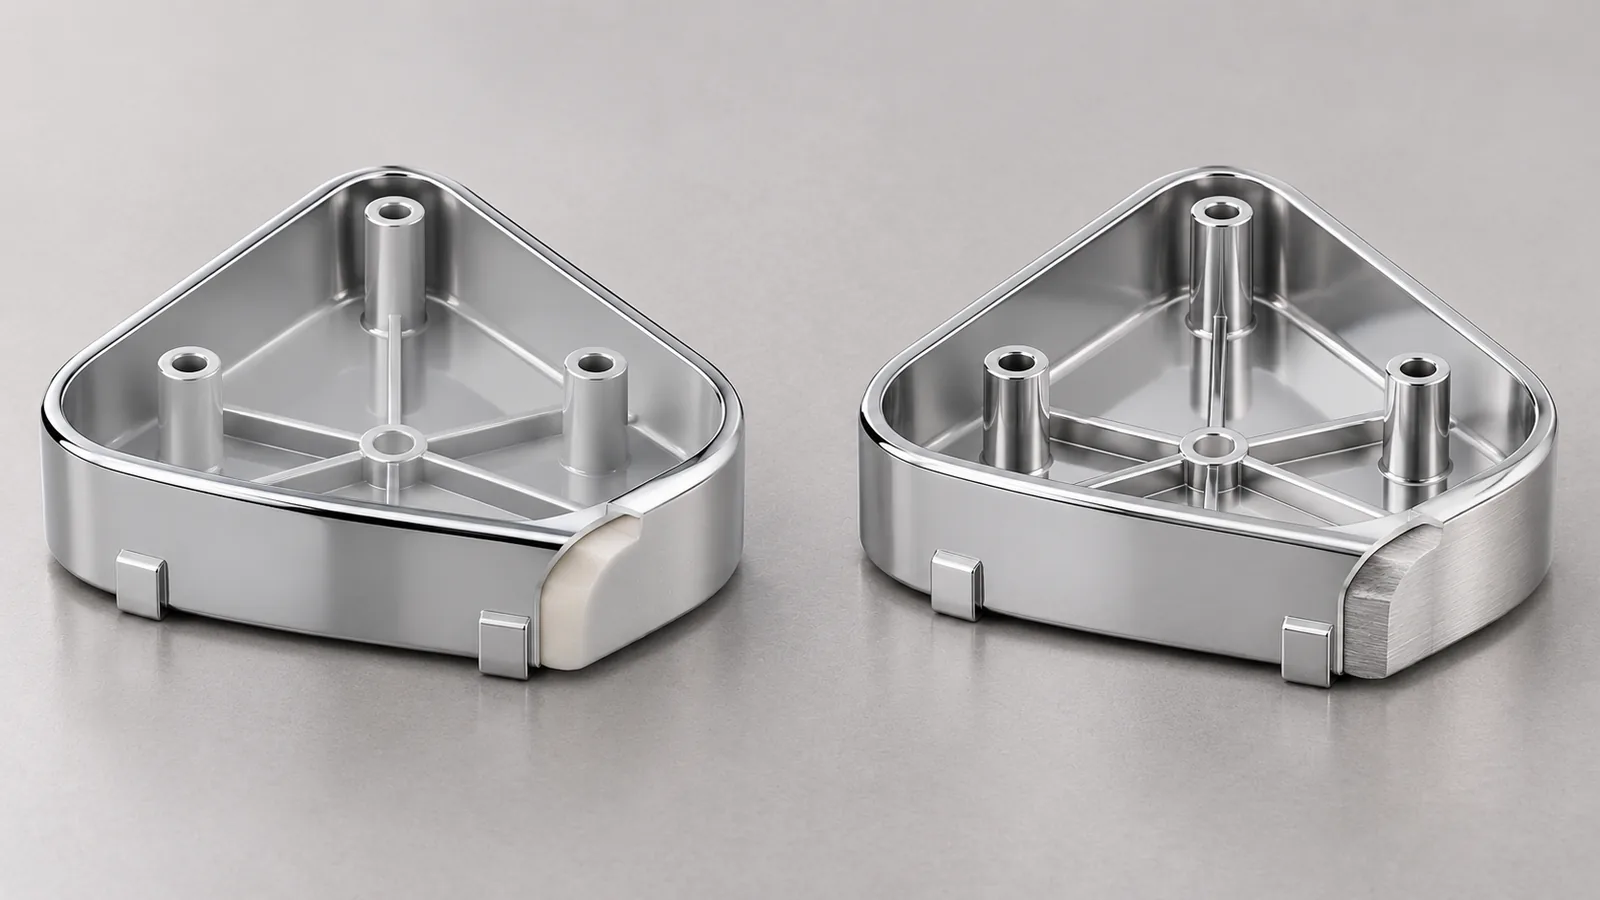
Plating plastic vs metal bathroom accessories is not a choice between identical materials with different names: plating a plastic component requires a substrate-specific pretreatment and metallization route, while plating a metal component begins with a conductive metal substrate and its own preparation. Buyers coordinating an ABS cover with metal hardware should specify each substrate separately, ask each responsible specialist to describe its process, and approve the parts together against a shared visual reference. A matched appearance does not prove matched structure, adhesion, corrosion behavior, or service life.
Why does the substrate change the plating decision?
Plating deposits metal onto a surface, but plastic and metal do not present the same starting surface. A metal substrate is electrically conductive and is prepared through a process chosen for its alloy, surface condition, contaminants, geometry, and desired layer system. Plating on plastic must first make the selected polymer surface suitable for metallization. The supplier’s preparation and activation route is therefore a central part of the process, not a minor variation of metal plating.
Plating plastic vs metal bathroom accessories is relevant when a product family combines materials. A molded cover, trim piece, handle, or decorative insert may be plastic, while the support, bracket, or fastener is metal. A buyer may want those parts to look coordinated. The visual objective does not erase the different substrates or the separate process controls required to achieve it. The buyer should identify the exact resin or metal grade and then ask the appropriate finishing supplier to confirm which routes are feasible for each one.
Do not assume that every ABS grade, blend, molded condition, or geometry can be plated simply because suppliers offer plating on plastics. Atotech describes processes for selected materials including ABS and certain blends, and explicitly presents multiple pretreatment or metallization options. That establishes that specialist processes exist for defined material families; it does not establish that every grade or part is suitable. A supplier must confirm the actual resin, molding condition, surface, part geometry, and intended finish. A buyer should record the resin maker and grade when available, rather than writing only “ABS.”
The same caution applies to metal parts. “Metal” does not tell a finisher whether the item is stainless steel, brass, zinc-based die casting, or another substrate. The material, fabrication, polishing, welds, casting porosity, and prior treatments can influence preparation. The plating supplier should identify the substrate it is quoting and list any assumptions. If the buyer changes the alloy or manufacturing route, the existing finish approval may no longer be representative.
There are two separate approval questions. First, can each substrate and geometry receive a feasible finish system? Second, can the finished components achieve an acceptable coordinated appearance and product performance for the defined use? A supplier may be able to plate both plastic and metal but still produce slight color or gloss differences because the substrates, surface profiles, preparation, or layer systems differ. The buyer must evaluate the assembled product under agreed conditions and determine whether the visual variation is acceptable.
The source distinction matters commercially as well. A metal hardware manufacturer may fabricate the metal components, while a specialist finishing supplier handles decorative metal plating and another specialist handles plastic pretreatment and plating. The product owner or importer coordinates the approved finish target, samples, and change control. Koitor’s verified role supports discussion of custom metal hardware, drawings, and sample coordination; in-house plastic plating, plastic molding, and plating equipment are not confirmed. Do not assign unverified process capability to Koitor or treat this article as a process qualification.
How does plating on plastic work at a high level?
Plastic plating is a specialist process family rather than a single universal recipe. The finishing supplier evaluates the polymer and part, prepares the surface using a route designed for that material, establishes the required conductive or metallized layer path, and applies the selected metallic finish. Some suppliers describe conventional and direct metallization technologies, and their product literature identifies different treatment families for selected plastics. The exact sequence, chemistry, parameters, and environmental controls belong to the qualified process provider; this guide does not prescribe a chemical recipe.
The buyer’s role is to provide enough information for that provider to assess the actual component. Supply the resin grade and source, molding conditions or supplier information if available, part drawing, cosmetic face map, gate and parting-line locations, assembly interfaces, and sample. If the part is already molded, identify whether the sample represents the intended production resin and mold finish. A plated sample on a different resin or surface may help discuss appearance but cannot automatically prove production readiness.
Geometry deserves early review. A plastic part may contain recesses, ribs, thin sections, sharp transitions, snap features, deep pockets, or areas that contact another component. The finishing supplier should review access and process suitability, while the molder should review moldability and the surface condition required for the selected finish. The same feature can matter differently to both suppliers. A recessed face may be a cosmetic target, an assembly seat, or both; mark its function so no one assumes it can be modified without consequence.
The buyer should ask what layer system is proposed and what each stage is intended to achieve. It is not enough for the quote to say “chrome plastic.” Request a supplier-controlled description of the finish route and its visible layer, plus any underlayers or pretreatments the supplier considers important to the specified product. The buyer does not need to dictate chemistry without expertise. The goal is to preserve enough information to compare offers and ensure that the approved sample and production order refer to the same system.
Metal-part plating has a different starting point. The finisher must identify the alloy and surface condition, preparation requirements, polishing or buffing scope where applicable, layer stack, masking, contact points, and appearance criteria. If the metal piece has welded joints, folds, cavities, or polished faces, review those details before quoting. A design approved for a plastic component cannot simply be transferred to metal, and a finish schedule for one alloy is not automatically suitable for another.
The processes also create different manufacturing interfaces. Plastic can be molded with features that help assembly, while a metal component may be fabricated and polished before finishing. The resulting plated builds can affect clearance, snap engagement, screw holes, seating, or the appearance at a seam. The buyer should identify critical fit features on the drawing and ask suppliers to state whether they will be plated, masked, or checked after finishing. Make the functional fit decision with finished components, not only bare samples.
How should buyers coordinate appearance across plastic and metal?
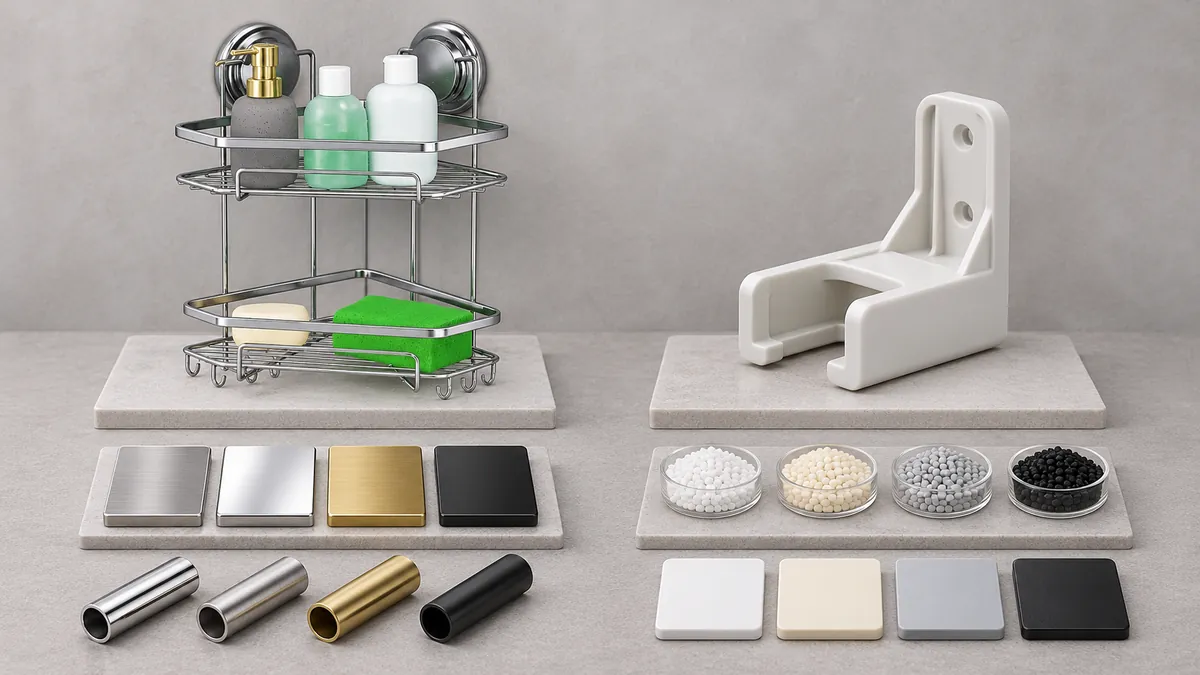
Create a single product-level finish brief that applies to the assembled product, then add substrate-specific process sections. At product level, define the intended color family, brightness or gloss character, visible contrast, texture, and viewing context. At the component level, state the resin or metal, supplier, proposed finishing route, layer stack reference, cosmetic surfaces, masked features, and evidence. This arrangement helps teams coordinate the visual goal without pretending that both substrates share one processing specification.
Use actual paired samples whenever possible. Obtain one finished sample of each substrate and assemble or position them as they will appear in the product. Review them side by side and in the intended orientation. Note which surface is most visible, whether one part reflects more light, whether the plastic part has a different curvature or texture, and whether seams make a mismatch more noticeable. A finish card can help compare a color family, but it does not replace evaluation on the real part geometry.
Agree on sample identification. Each piece should show supplier, substrate, resin grade or metal designation, part revision, finish system reference, sample date or lot identifier if available, and approval status. Keep a controlled master sample or documented reference under conditions that protect it from abrasion, cleaning, and fading. If the buyer approves by photo because physical shipping is impractical, record that limitation and reserve physical confirmation for the next available sample. Images can shift color and gloss depending on display and lighting.
State the viewing method for visual comparison. The buyer should identify consistent lighting, distance, angle, background, and whether the parts are clean and dry. A change in those conditions can make the same surface appear different. If the project has a formal color instrument or standard, specify the method and responsible party; do not invent a tolerance or require a measurement the supplier cannot perform. The appearance acceptance method should match the product risk and be agreed before mass production.
Remember that matching color does not mean identical performance. Plastic and metal parts may experience different stresses, temperature, cleaners, impact, or moisture exposure. The buyer must define the application and ask the respective specialist to provide evidence appropriate to each substrate. Do not assume that the plastic part’s finish behaves like the metal part’s finish because both look chrome-like. Also do not make broad claims that one substrate will always be more durable or less expensive.
Use a paired approval record with separate acceptance rows:
| Approval field | Plastic component | Metal component |
|---|---|---|
| Base material | Resin maker and grade; molding revision | Alloy or material designation; fabrication revision |
| Proposed finish route | Specialist-confirmed pretreatment and plating system | Specialist-confirmed preparation and plated layer stack |
| Cosmetic surfaces | Visible faces, gate and parting-line zones | Visible faces, welds, polished areas and contact marks |
| Critical interfaces | Snap, seat, clearance, holes and mating surfaces | Threads, holes, mounting faces and assembly fits |
| Sample standard | Identified plated sample tied to molded revision | Identified plated sample tied to metal revision |
| Evidence and responsibility | Supplier, method and approval owner | Supplier, method and approval owner |
The comparison does not suggest that suppliers can always achieve identical color across substrates. It creates a decision record: which differences are acceptable, what evidence was reviewed, and who approves a change. If the owner wants the components to look indistinguishable, the finishing supplier should confirm feasibility and define the sampling method; the buyer should not write “perfect match” without a practical acceptance process.
What should a buyer request from each supplier?
Send the plastic-plating supplier the exact polymer grade, molded sample, drawing, intended finish target, production quantity, visible surface map, and information about prior molding or surface treatments. Ask the supplier to confirm that the material and geometry are candidates for its process, identify any limitations, and provide a proposed system description. Ask how it will identify the approved resin and molding revision on later orders. If a design change affects the surface or feature geometry, require the supplier to review whether the previous process approval remains valid.
Send the metal-plating supplier the exact alloy or substrate designation, fabrication drawing, current surface condition, sample, and requested layer system if the product owner already controls one. Mark polished and visible faces, welds, holes, threads, masking needs, and areas where rack marks may be acceptable. Ask the supplier to identify any preparation or geometry limitations and explain what sample will represent production. If the buyer is considering a different metal or finish route, make that alternative explicit and obtain approval before changing the product.
Both suppliers should receive a shared product context. Tell them which components appear together, where the part is used, which color or finish reference controls, what the cleaning or exposure requirements are, and which party owns final visual approval. This does not require disclosing confidential customer information. The importer can provide anonymized application details and controlled drawings, while restricting access to brand assets, customer data, and proprietary commercial details as appropriate.
Request a comparable quote scope from each supplier, but do not force the same process description onto dissimilar substrates. For plating plastic vs metal bathroom accessories, compare responsibilities, piece-price basis, minimum batch, setup or development charges, sample rounds, inspection and reports, packaging, freight, and exclusions. Ask whether a proposed price covers only finishing or also includes sorting, assembly, or protective packaging. If the metal fabricator coordinates the plastic finisher, identify any project-management or logistics scope separately rather than assuming it is included in the metal part price.
Ask for a sample plan with defined stages: early feasibility sample, appearance sample, production-intent sample, and approval reference if those stages are relevant. For each stage, state whether the same material, tooling, finish system, and geometry will be used as production. A prototype may be useful for checking assembly without proving final appearance. A color plaque may help select a finish without proving coverage on a deep recess. Identify what each sample demonstrates and what remains unverified.
Each supplier should describe its own quality evidence. That may include supplier process documentation, visual inspection, dimensional checks on specified interfaces, or tests defined by the project. The evidence must identify the part, revision, method, and acceptance criteria. Do not require a generic report simply to check a box, and do not accept a test report if it describes a different substrate or finish system. If no numerical acceptance limit has been established, ask the product owner or technical authority to define one before production rather than inventing a threshold.
How should buyers evaluate risks and acceptance criteria?
The main risk is assuming that the same decorative name guarantees the same physical finish. A product name such as “chrome” does not tell the buyer which substrate was plated, how it was prepared, which layers were applied, or how it was inspected. Record the complete supplier-defined route in the quotation or finish schedule. Use the approved sample as the visual target, but keep the process description and technical evidence linked to it.
A second risk is approving the plastic and metal parts separately without reviewing the assembly. Individually, each component may fall within its own supplier’s visual expectation, yet their reflectivity, hue, gloss, or texture may look inconsistent when installed next to one another. This is a coordination issue. The product owner must establish the acceptable product-level relationship and approve the paired samples under consistent conditions. If one component is hidden after assembly, define that before comparing it to visible pieces.
A third risk is changing the resin, alloy, molding tool, polishing sequence, finish supplier, or coating system without a documented review. These changes can influence the finished result or fit. Set a notification and approval trigger in the purchase documents. The supplier should identify changes that affect its process; the buyer should decide whether a new sample or evidence is needed. Preserve the revision, approval date, supplier, and disposition.
A fourth risk is vague evidence. A claim that a finish “passed testing” is not enough unless the buyer knows what was tested, on which substrate and sample, under what method, with what acceptance criteria, and by whom. The report should be relevant to the actual item. If the product owner requires a particular standard or test, verify that it applies to the market and application. This article does not define legal compliance or certify either a product or supplier.
A fifth risk is confusing decorative appearance with suitability for a bathroom environment. The bathroom is not a single exposure condition. A residential vanity item, a shower-exposed part, a hotel accessory, and a coastal property may have different cleaning, moisture, abrasion, or use expectations. State the actual application and ask the process specialists which evidence they recommend. Neither a plated appearance nor a material label alone proves long-term performance.
Cost comparison can also mislead. Plastic and metal plating may have different preparation costs, minimum quantities, yield assumptions, part handling needs, and supplier economics. The buyer should compare the full scope for each component and the combined supply plan, not assume that plating plastic is automatically cheaper because the base resin is light, or that metal plating is always more expensive. No universal unit-price comparison can be derived without actual supplier quotations for the specified part and volume.
Finally, do not treat the finisher’s marketing material as project acceptance. A supplier portfolio can show that a technology exists for a material family or application, but only the responsible supplier can confirm the specific grade, geometry, finish stack, production route, and evidence for the buyer’s part. Use public references to formulate questions, not to replace a technical review or supplier approval.
How should the buyer manage samples, changes, and production release?
Create one product-level approval record with separate component records. The product record names the assembled configuration, finish target, application, and approval owner. Each component record identifies its own drawing revision, substrate, supplier, finish route, sample, interfaces, inspection method, and decision. This prevents a buyer from treating two components as one undifferentiated “chrome finish” line item.
At sample review, use a written disposition: approved, approved with specified limitation, or rejected with corrective action. Identify the viewed surfaces and the evidence reviewed. If a color difference is accepted, state the permitted relationship or reference sample rather than relying on a meeting memory. If one supplier cannot meet the target, route the issue to the product owner for a design or finish decision. Do not authorize production based only on a verbal compromise.
Before production, tie the purchase order to the approved drawing revision, material designation, finish system references, color or visual standard, packaging, inspection requirements, and supplier responsibilities. If multiple suppliers are involved, define who assembles, who protects the surfaces, who performs final appearance review, and who controls shipment release. A supplier who only plates a component should not be assumed to validate the entire finished product.
Packaging should protect the approved surfaces during handling and transport. Ask the responsible supplier to identify contact points, separators, bag or wrap materials, and orientation that avoid rubbing or contamination. Review the package with both substrates in the intended assembled or packed arrangement. A scratch created after finishing can be a logistics or packaging issue rather than evidence that the plating route itself is defective; preserve the chain of custody and inspection timing when investigating a claim.
For a reorder, compare the supplier’s current material and finish documentation with the approved record. Confirm that the resin grade, metal substrate, finishing source, and part revisions remain controlled. If the supplier proposes a new chemical system, process source, resin, or alloy, document why and what additional sample or evidence is required. Do not assume that the same color name on a new process is equivalent to the existing sample.
If a quality issue is reported, collect the part identifiers, supplier and lot, photos under consistent lighting, assembly context, storage and cleaning history if available, and the exact approval criterion. Keep the failed sample and reference sample. Ask each supplier to investigate within its responsibility and avoid assigning blame before the facts are reviewed. A plastic-plating issue and a metal-plating issue may have different causes even if the visible symptom is similar.
Buyer checklist before approving plated plastic and metal components
- Identify the exact resin grade and metal substrate; do not use only the word “plastic” or “metal.”
- Provide controlled drawings, 3D data where available, samples, visible-face maps, and mating-interface information.
- Ask the plastic-plating supplier to confirm resin and geometry suitability for its proposed process.
- Ask the metal-plating supplier to confirm substrate preparation and its proposed layer stack.
- State the product-level visual goal and define substrate-specific process records separately.
- Mark gates, parting lines, welds, polished faces, recesses, holes, threads, rack contacts, and critical fit surfaces.
- Review paired finished samples in the assembled orientation using agreed lighting and a controlled reference.
- Request a sample plan and clarify which stage proves appearance, fit, or other specified criteria.
- Ask each supplier for relevant evidence tied to the actual material, part revision, process, and acceptance method.
- Compare quoted setup, piece price, order minimum, sample fees, inspection, packaging, freight, and exclusions.
- Define change-notification and reapproval triggers for resin, alloy, geometry, process, or supplier changes.
- Record the approved supplier scope, reference sample, inspection responsibility, and production release owner.
Use this list to make the RFQ complete, not to force an unverified technical answer. If the resin is not selected, request a feasibility assessment and proposed options. If the metal grade is uncertain, confirm it with the product engineer. If a finish test or legal requirement applies, verify its current scope with the qualified authority for the destination market.
Perguntas frequentes
Can ABS and metal have a similar plated appearance?
They can be developed toward a coordinated visual target, but buyers should confirm this with paired samples and a defined review method. The different substrates and preparation routes mean that identical appearance or performance should not be assumed from the process name.
Is every ABS grade suitable for plating?
No. Specialist suppliers describe processes for selected plateable plastics and material families. The actual resin grade, molded surface, geometry, and process must be reviewed by the responsible supplier.
Does plating plastic use the same process as plating metal?
No. A plastic surface needs its own pretreatment and metallization route. Metal preparation depends on the alloy and fabrication condition. The supplier should identify the route for each component.
Does a chrome-like appearance prove the part is metal?
No. The visible appearance does not establish the underlying substrate. A buyer should keep material identity and finish description in the component specification and supplier records.
Can a metal finish sample approve a plastic component?
It can serve as a visual reference for a design discussion, but it does not prove that the plastic component’s process or performance is acceptable. Approve a representative sample on the actual substrate and geometry.
Does the same finish name mean the same coating stack across suppliers?
Not necessarily. Request a written system description and identify the sample tied to that system. Different suppliers may use different substrate preparation, layers, or process controls.
Who should approve a coordinated finish?
The product owner or designated technical decision-maker should approve the assembled appearance and project requirements, with each specialist supplier confirming its own process scope. The approver should be named in the project records.
Does Koitor plate ABS and metal bathroom accessories in-house?
The current approved capability information does not confirm in-house plastic plating or plating equipment. Koitor’s verified scope includes custom metal hardware manufacturing and buyer-supplier coordination; confirm specialist finishing responsibility for each project.
Technical references
- Atotech: Plating on plastics — supplier information on material families and plastic metallization technologies.
- Atotech: Sanitary industry — supplier examples spanning plastic and metallic substrates and decorative finishes.
- See Koitor Hardware’s OEM manufacturing information for verified metal hardware context.
Coordinate Your Component Finish Brief
Share the controlled resin and metal specifications, drawings, visual references, and paired-sample requirements so the relevant hardware and finishing suppliers can review the project scope.
OEM / MARCA PRÓPRIA
Transforme este guia de fornecimento num resumo do produto
Indique o produto pretendido, as dimensões, o acabamento, a quantidade a encomendar e os requisitos de embalagem. A sua equipa receberá uma análise prática da viabilidade de fabrico antes da apresentação do orçamento.


 English
 Español
 Português
 Français
 Deutsch
 العربية