

Roughness cutoff filter stylus tip measurement should be agreed before buyers compare supplier reports for a polished metal part. A roughness value is produced by a measurement method: the stylus, filter, cutoff, evaluation length, trace direction and parameter all shape what is captured and reported. If two suppliers use different settings, apparently different numbers may reflect method differences as well as surface variation. For bathroom and home-storage hardware, buyers need a comparable method that can be applied to the product’s actual geometry and finish zones.
This guide helps importers and product developers define a supplier-facing measurement plan without selecting arbitrary settings. It is not a substitute for the current applicable standard, instrument manual or qualified metrology advice. A standard specifies terminology and operators; the design authority still decides which surface characteristic matters and what acceptance limit is appropriate. Koitor’s confirmed scope includes grinding and polishing metal hardware, while access to a particular profilometer, stylus or accredited laboratory must be confirmed for each project.
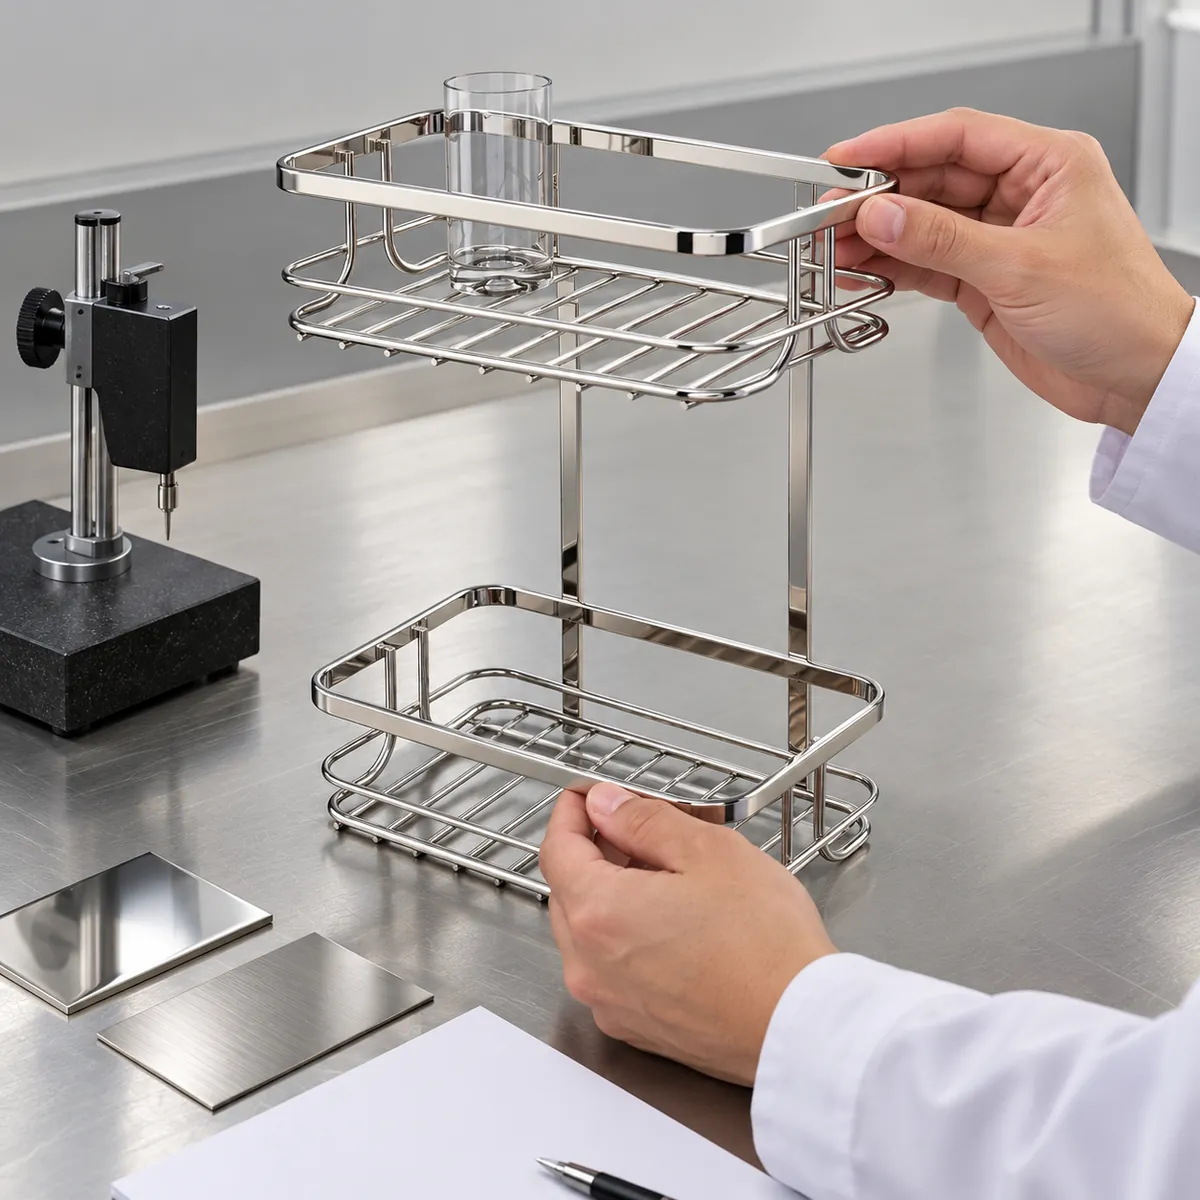
What do cutoff, filter and stylus tip control?
A stylus instrument traces a surface profile and processes the signal according to the selected measurement and filtering approach. The stylus tip interacts with peaks and valleys; its geometry and condition influence which surface details it can follow. A filter separates profile components according to specified parameters, and a cutoff is part of that specification. These controls are not interchangeable labels for a single “roughness setting.”
A buyer does not need to become an instrument specialist to request comparable evidence. The buyer does need to ensure that both parties identify the governing method, parameter, filter/cutoff, stylus configuration and evaluation length or corresponding specification elements. ISO 21920 is the current profile-surface-texture standards family: ISO 21920-2 covers terms, definitions and parameters, while the related parts address indication and specification operators. Always confirm the applicable edition and drawing callout rather than assuming an older default applies.
Mitutoyo’s technical material shows that cutoff and stylus-tip radius are related considerations in instrument selection. That does not create one universal setting for every bathroom rack. The selected method depends on the texture scale, material, geometry, required parameter and intended decision. A measurement plan should state how the settings were chosen and who approves them.
Why is the measurement method part of the buyer specification?
A supplier’s Ra or Rz result can appear authoritative because it has a unit and decimal places. But a number without the method context is incomplete. The stylus can bridge narrow valleys, a filter can separate profile components, and the trace direction can interact with a directional brushed pattern. The report should therefore identify the method inputs that affect comparability, not simply the final value.
For a polished or brushed bathroom accessory, the measured point also matters. A flat coupon may not represent a curved rail, a welded junction or a narrow wire surface. Buyers should identify which product surfaces drive function or appearance and confirm that the instrument can access them without unstable support or edge effects. If the geometry prevents a valid stylus trace, the buyer may need a different measurement approach or a representative flat witness sample, clearly labeled as a proxy rather than the product itself.
An acceptance limit also needs a reason. It may be tied to a functional interface, a drawing note, a validated process requirement or a controlled appearance sample. Do not infer hygiene, corrosion resistance, cleanability or consumer perception from a roughness value alone. Those properties depend on additional material, finish, exposure and use factors.
How should suppliers make results comparable?
Start with a controlled drawing or finish specification. Identify the part, revision, material and surface zone. Name the profile parameter and governing standard or method, then specify the measurement settings that are material to the result. If the buyer does not know which stylus radius or cutoff is appropriate, ask the metrology owner to propose the method and rationale for the actual texture and measurement range.
The buyer should also define trace orientation. For directional finishing, a trace parallel to the grain can produce a different profile from a trace across it. State whether measurement is along or across the lay, or identify both when the acceptance question requires it. Record the actual trace location, direction and number of traces according to the approved plan. Avoid allowing the inspector to choose any convenient location after seeing a result.
Confirm instrument capability and condition. Ask whether the stylus is suitable for the material and profile, whether the tip is clean and undamaged, whether the instrument is verified according to its operating procedure, and how the part is supported. This article does not prescribe an instrument verification interval or calibration requirement; follow the instrument owner’s quality system and project requirements.
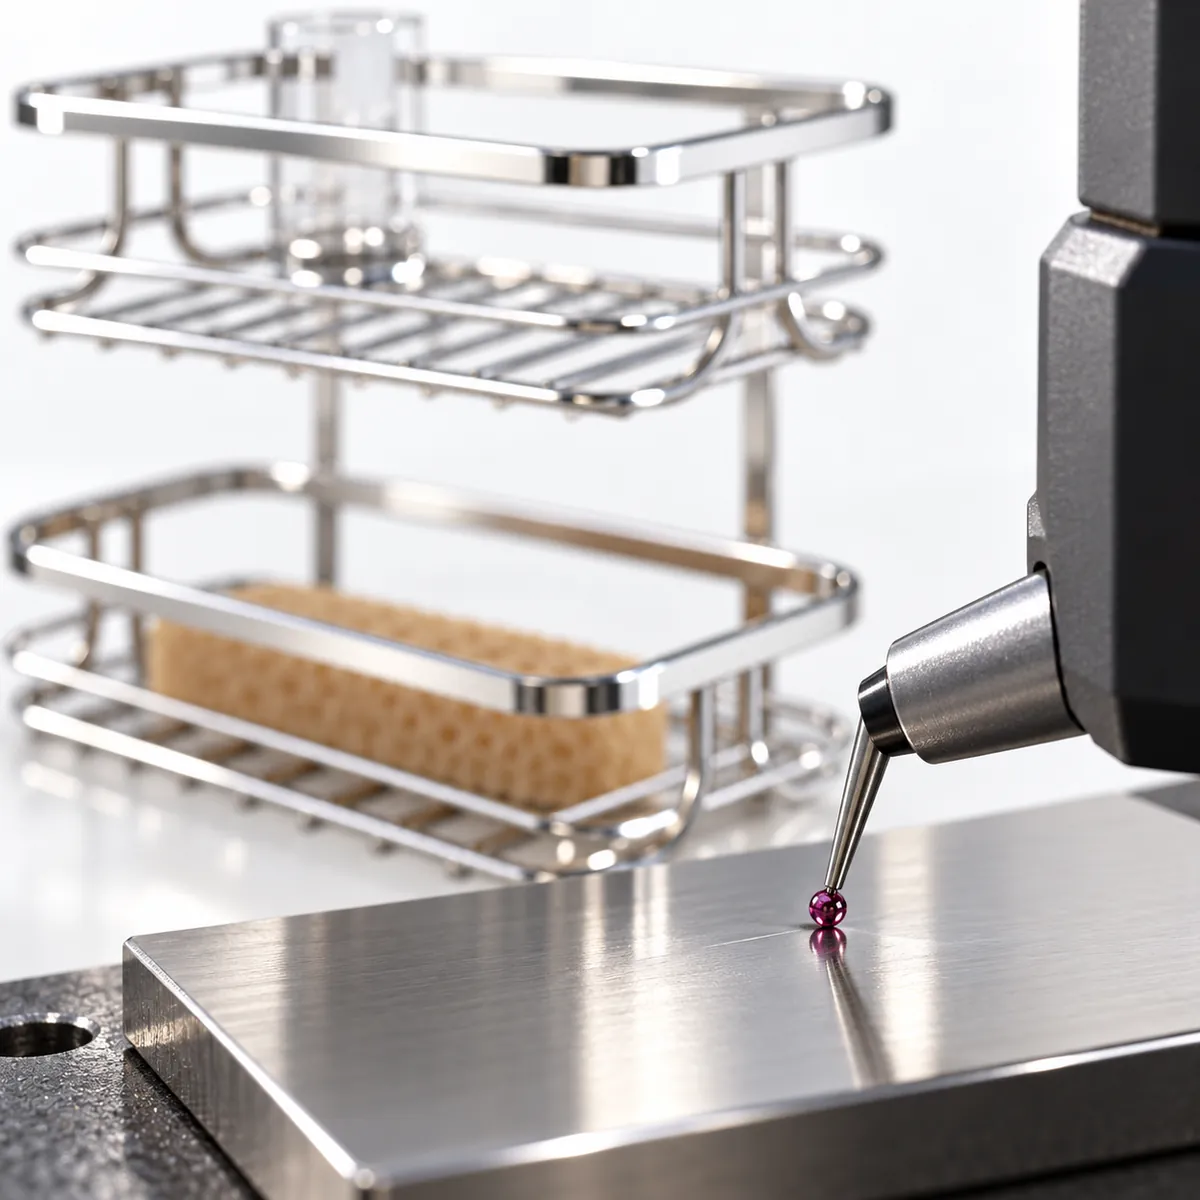
| Method input | Why it matters | Buyer record | Common comparison risk |
|---|---|---|---|
| Parameter and standard | Defines what profile characteristic is reported | Parameter, method and applicable edition | Comparing different parameters as if they were equivalent |
| Cutoff/filter | Changes profile separation and evaluated content | Filter type and selected cutoff or operator | Settings differ between supplier reports |
| Stylus configuration | Affects access to and capture of profile features | Tip geometry and condition where relevant | Different tips interact differently with fine features |
| Trace path and direction | Relates measurement to product location and lay | Marked zone, orientation and support | Trace orientation or point selection changes the result |
Where should buyers measure on a bathroom or storage part?
Select a location that represents the requirement and can be measured reliably. A broad flat section may provide a suitable trace, but the buyer should consider whether the finished product has a visible face with different process history. For a wire basket, the curved wire, weld, bend and adjoining surfaces can each finish differently; an instrument designed for a flat test piece may not reach each area in the same way.
If a small component is used as a witness coupon, document how it relates to the production part: same material lot or grade, same finishing route, same process stage and same relevant orientation, where these are controlled. A coupon can improve access, but it cannot automatically stand in for every product geometry. The buyer should approve the proxy arrangement before using it as acceptance evidence.
For an accessible product surface, show the measurement zone on a drawing or photograph. Keep the stylus away from edges or discontinuities unless the specification explicitly intends to evaluate them and the method supports that measurement. If a weld transition is the concern, define a separate inspection approach rather than placing a stylus across a complex joint and interpreting the reading as a standard surface roughness value.
Use a stable support that does not introduce vibration or deflection. The supplier should explain how the part is held and whether that support changes the surface or geometry. Record the sample state: before or after coating, after polishing, assembled or unassembled. A roughness reading on bare metal does not describe a later applied finish unless the buyer has specifically defined that relationship.
What should appear in the supplier measurement report?
A concise report should let a second reviewer reproduce or interpret the result. Ask for:
- Part number, drawing and finish revision, material description and sample ID.
- Measured surface zone and trace direction, with a photograph or marked drawing where useful.
- Parameter, profile method and governing standard or specification revision.
- Filter type and cutoff/operator, stylus type or tip radius, and evaluation length or equivalent method inputs.
- Instrument identification and the measurement owner’s relevant verification status.
- Part support or fixture condition and whether the sample was coated, polished, assembled or otherwise prepared.
- Individual readings and the agreed summary method, rather than only a selected best result.
- Acceptance limit source, sample reference or drawing requirement and approval owner.
- Any deviation from the specified method and the reason it was necessary.
Do not demand hidden instrument settings that the supplier cannot access or that do not apply to the chosen standard. Instead, agree which method inputs are necessary for a valid comparison and how the supplier will record them. If the instrument uses a named specification operator or stored program, identify the program revision and retain its key settings in the report.
When suppliers disagree, first compare the measurement method, not just the numerical value. Check whether the same parameter, filter, stylus, trace direction, evaluation length, sample state and location were used. If not, a controlled remeasurement may be needed before concluding that the product finish changed. Keep initial and corrected reports so the method adjustment remains transparent.
How do buyers set limits without over-specifying?
A limit should reflect the buyer’s functional or appearance need and be technically measurable on the product. If the design team has no reason to control a particular surface parameter, adding a number may create cost and disputes without improving the product. If the parameter is important, define the method and acceptance basis together. A limit disconnected from a measurement method is not a complete specification.
For an appearance-driven finish, a controlled physical sample may be more useful than a single roughness value. A buyer may use both: a sample for overall visual acceptance and a numeric parameter for a specific process or functional surface. Make clear which governs if they disagree. Do not promise that a roughness measurement alone predicts corrosion behavior, cleanability or durability.
Supplier quotations should be compared using the same measurement scope. One offer may include a traceable profilometer report and representative part sampling, while another may include only a visual check. The buyer should state whether instrument measurement is required at development, first article or ongoing production, and who pays for any additional lab work. Where no suitable instrument is confirmed, mark that as a project decision rather than implying Koitor owns a particular advanced inspection tool.
Common errors in roughness cutoff filter stylus tip measurement
One error is writing “Ra required” but leaving the filter, cutoff, trace direction and surface zone undefined. Another is comparing a result measured with one stylus configuration to a result measured with another without confirming comparability. A third is accepting a supplier report with only a parameter value and no method or location details.
Avoid selecting a cutoff from a generic table without checking the applicable standard and surface condition. Avoid assuming that a sharper stylus is automatically more accurate; tip condition, geometry, material and instrument capability all matter. Do not treat a polished surface coupon as equivalent to a curved product rail without documenting the relationship.
It is also easy to over-interpret decimals. More digits do not guarantee better measurement or better agreement. The measurement system, trace location and method need to support the reported resolution. If a result is close to an acceptance limit, the buyer and supplier should consider measurement uncertainty and the agreed decision rule rather than rounding a borderline value into compliance.
Finally, do not mix roughness with waviness, form, gloss or visual texture. Those are related surface characteristics but not identical. If the buyer sees a repeating ripple or an uneven reflection, the measurement question may require another parameter or method. Describe the observed concern and ask the qualified metrology owner which tool can answer it.
Buyer checklist and FAQs
Before accepting a supplier roughness report, verify that the roughness cutoff filter stylus tip measurement method has been aligned and that it:
- Identifies the part, revision, sample and finish state.
- Marks the measurement zone and trace direction.
- Names the parameter, applicable method/standard and revision.
- Records filter, cutoff, stylus configuration and other required method inputs.
- Uses support and instrument access suitable for the actual product geometry.
- Shows individual results and a defined summary method.
- Links the acceptance limit to a drawing, validated requirement or approved sample.
- Explains any deviation and obtains approval before using a substitute method.
Does a smaller cutoff always mean a more accurate result?
No. The setting must fit the method, texture and measurement purpose. An unsuitable cutoff can make results less comparable rather than more accurate.
Can one roughness reading represent a whole basket?
Not automatically. Surface location, geometry, finishing history and trace direction may vary. Define representative zones and sample quantity for the project.
Is stylus tip radius just an instrument detail?
No. Tip geometry affects how the stylus interacts with surface features and must be suitable for the method and texture being evaluated.
Does Ra prove that a bathroom finish is corrosion resistant?
No. Roughness is only one surface descriptor. Material, finish system, contamination, exposure and other factors require separate evaluation.
Koitor supports custom metal hardware development from drawings and samples, including grinding and polishing processes. Share the relevant drawing callout, finish reference, measured zone and supplier report requirements through Koitor’s contact page, or review the OEM manufacturing overview. Specific instrument access and acceptance limits must be confirmed per project.
Technical references: ISO 21920-2 profile surface texture parameters and Mitutoyo surface roughness tester quick guide. Check the current applicable standard edition and instrument documentation before establishing a controlled method.
Align a finish measurement method
Share the drawing callout, surface zone, reference sample and report needs for a project-specific discussion.
OEM / PRIVATE LABEL
Turn this sourcing guide into a product brief
Share your target product, size, finish, order quantity and packaging requirements. Your team receives a practical manufacturability review before quotation.
 English
 Español
 Português
 Français
 Deutsch
 العربية