Importers who buy a powder coated shower caddy often discover the hard way that “matte black powder coat” is not a complete specification. Humidity, soap film, and daily impact punish thin edges, weak adhesion, and packaging rub marks long after the carton looks fine on arrival. This guide is a buyer and OEM defect catalog: ten named coating defects, photo-spec labeling, CTQ language, and clear accept / rework / reject rules for wire bathroom storage—not a rewrite of process pillars on DFT, pretreatment, or Faraday cage application technique.
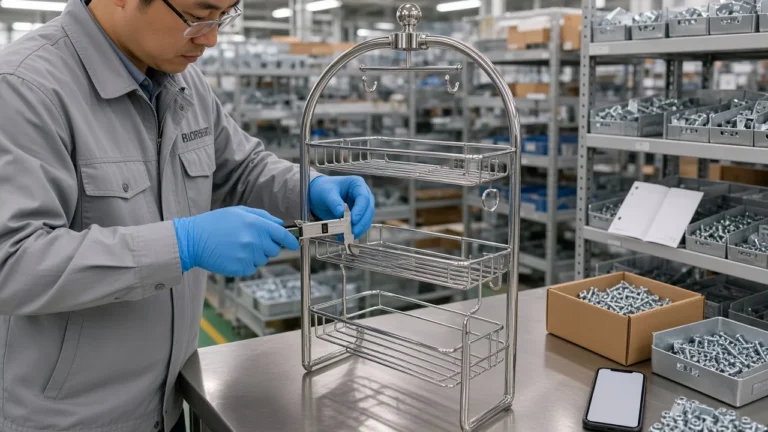
Use it beside your drawing package and IQC checklist. Pair the defect names below with the process controls in our humid-bathroom powder coating guide when you audit a line, and keep sampling decisions aligned with your AQL plan for wire bathroom hardware. Photos in this article are generic visual starting points for RFQ language; they do not claim that every SKU ships from one factory.
Table of Contents
- Why Coating Defect Language Matters for Wire Bathroom Hardware
- How to Read a Powder Coated Shower Caddy Defect Spec
- 10 Coating Defects Buyers Must Name and Photo-Spec
- Accept, Rework, or Reject: Decision Rules for IQC
- RFQ Checklist Language for Humidity Durability and Adhesion
- FAQ: Powder Coated Shower Caddy Defects and Specs
- Send Your Powder Coated Shower Caddy Spec for Review
Why Coating Defect Language Matters for Wire Bathroom Hardware
Wire shower caddies combine dense weld grids, sharp cut ends, hanging hooks, and thin-section frames. Those geometries make powder film behavior uneven even when the spray booth looks busy. A buyer who only writes “powder coat, black, outdoor grade” leaves the factory free to ship orange peel on open faces, edge thin film on hooks, and packaging abrasion that becomes underfilm creep after a few wet months.
Retail returns rarely say “Faraday cage.” They say “rusted,” “paint peeling,” “color not matching,” or “scratched out of box.” Your RFQ and acceptance plan must translate those complaints into named coating defects with measurable CTQs. That is the job of this article. Process depth—wash chemistry, DFT windows, gun settings—belongs in the companion process pillar on humid-bathroom powder coating DFT, pretreatment, Faraday cage, and packaging. Here we stay on what buyers must call out, photograph, and disposition.
What “good enough” looks like in a wet bathroom
A durable powder coated shower caddy in a humid bathroom keeps film integrity at edges and welds, resists soap and condensate, and survives install handling without chip-outs that expose bare steel. Color stays within an agreed ΔE or visual limit under a defined light source. Crosshatch adhesion on representative flats and wire faces meets the grade you wrote, not a verbal “strong adhesion.” Salt-fog or cyclic humidity exposure—if you require it—is tied to substrate, pretreatment, and film system, not a random hour number copied from another product family.
Where OEM cost pressure creates hidden risk
Common commercial pressure points include thinner film to save powder, shorter cure to raise throughput, softer packaging to cut cube cost, and skipping adhesion or DFT checks on dense weld corners. Each pressure point maps to one or more of the ten defects below. If your PO does not name the defect, photo evidence, and disposition, IQC will argue taste instead of contract.
Importer failure modes that start as “coating complaints”
Most coating returns for bathroom wire goods cluster into five commercial stories: rust rings on hooks after a few months, paint chips during install, color mismatch across a set, dull or dirty-looking texture that photographs poorly, and scratched units out of the box. Each story maps to one or more named defects in this catalog. If your claim system only codes “finish issue,” you cannot trend root causes or hold a supplier to a CAPA that cites DEF-03 versus DEF-10.
Private-label teams also need defect language for chargebacks and for comparing two factories that quote the same RAL-ish black. Without photo masters, the cheaper quote often wins on sample day and loses on the third production lot when orange peel and edge thin film return. Treat the powder coated shower caddy finish as a documented product characteristic, not a commodity spray service.
Boundary with the process pillar
This post does not re-teach pretreatment chemistry, target DFT engineering, Faraday cage gun technique, or packaging foam selection. Those controls belong in the humid-bathroom process pillar. Buyers still must know when a defect points upstream: pinholes and poor adhesion often implicate cleaning and outgassing; Faraday corner rust start implicates deposition and hanging; packaging abrasion implicates nesting and bagging. Use defect IDs in the nonconformance report, then open the process checklist with the factory engineer.
How to Read a Powder Coated Shower Caddy Defect Spec
Write every coating requirement as a closed loop: defect name, where it is inspected, how it is measured or photographed, severity class, and disposition. Ambiguous words such as “nice finish,” “no rust soon,” or “good powder” fail under dispute. For a powder coated shower caddy program, treat coating as a CTQ family equal to weld integrity and dimensional fit.
Photo-spec labeling that survives email and WhatsApp
Golden-sample photos work only when each image carries a label block: SKU, finish code, viewing distance, light type (D65 / daylight / shop LED), magnification if macro, and defect ID from your catalog (for example, DEF-03 Edge Thin Film). Mark accept / borderline / reject on the same frame or an adjacent annotated crop. Store the labeled set in the PPAP or first-article pack so production IQC is not comparing against a faded WeChat screenshot.
Adhesion and corrosion wording that matches official standards
For film adhesion on metallic substrates, buyers commonly cite ASTM D3359 tape-test methods (Method A X-cut or Method B crosshatch) and a minimum classification such as 4B or 5B on defined locations. Note that ISO 2409 is a related cross-cut adhesion method with its own classification scale; do not mix rating numbers across ASTM and ISO without stating which standard applies. For salt-spray apparatus practice, cite ASTM B117 as the chamber practice—not as a pass/fail by itself. Duration, scribe, evaluation method, and acceptance limits belong in your product specification. For broader coating-system context in corrosive service, NIST’s overview on coatings for corrosion protection is a useful official background reference when educating non-coating stakeholders; it is not a shower-caddy product standard.
CTQ table starters for RFQs
Minimum CTQs for most powder coated shower caddy RFQs include: cured DFT window on flats and edges; adhesion grade and method; visual defect catalog with photo limits; color standard and ΔE or visual matching rule; cure verification (metal temperature / time, not only oven setpoint); and packaging abrasion criteria after drop or vibration simulation if you ship densely packed cartons. Add humidity or salt-fog only when your channel truly needs it—and when you can fund representative specimens, not just flat panels that ignore wire grids.
Documentation that survives staff turnover
Buyer teams change; factories change inspectors. A powder coated shower caddy program that lives only in chat threads will drift. Keep the defect catalog, photo masters, and CTQ table in a controlled folder with revision dates. Require suppliers to echo the same DEF IDs on their IQC sheets. When a new merchandiser asks why a lot was rejected, the photo-spec should answer in one page.
If you run dual sourcing, freeze the catalog before awarding the second tool. Competing plants should not invent local nicknames for orange peel or edge thin film. Harmonized language is how you compare true process capability instead of comparing who writes the friendlier inspection report.
10 Coating Defects Buyers Must Name and Photo-Spec
Name these ten defects in the purchase specification for every powder coated shower caddy finish. Keep the IDs stable across SKUs so IQC and suppliers share one vocabulary. Severity can differ by retail tier, but the names should not.
For each defect, keep four fields in your workbook: definition, primary buyer risk, measurement or photo method, and default disposition. The narratives below are starting points for that workbook. Adjust severity for hospitality versus mass retail, but keep IDs and photo geometry consistent so multi-factory programs stay comparable.
Also record whether the defect is judged on the finished assembly, on a coating coupon, or both. Wire shower caddies hide risk when coupons are flat panels that never see dense grids. Prefer production-representative pieces for visual CTQs and, when practical, for adhesion spots agreed at first article.
1. Orange peel
Definition: textured, dimpled film surface resembling citrus skin on open faces or large flats. Causes often include film too thick, powder flow/gel imbalance, or cure profile that does not allow adequate flow. Buyer impact: looks “cheap” in retail photography and can trap soap residue. Spec tip: define viewing distance (for example, 50 cm under D65) and whether light orange peel is allowed on non-facing wires. Photo-spec: side-by-side accept / reject under the same light. Disposition: usually rework by strip and recoating if color and DFT still allow; cosmetic-only lots may be downgraded with buyer approval.
2. Pinholes
Definition: fine voids that expose substrate or leave microscopic moisture paths. On a powder coated shower caddy, pinholes near welds and cut ends are high risk in humidity. Causes include outgassing from steel or weld slag, moisture in powder, or contamination. Spec tip: zero tolerance on customer-visible faces for mid/high retail; allow limited count on hidden hanger backs only if sealed and documented. Disposition: reject for visible pinholes on wet-zone faces; do not “touch up” with paint pens if you claim powder integrity.
3. Edge thin film
Definition: DFT on sharp edges, hook tips, and wire crowns below the minimum, often while flats still pass. This is one of the most common field-rust starters on wire bathroom hardware. Spec tip: require DFT readings on defined edge points, not only panel coupons. Photo-spec: macro of hook tip and shelf-wire crown with gauge reading in frame when practical. Disposition: reject if below minimum on CTQ edges; partial rework only if strip/recoat is approved and adhesion on rework is revalidated.
4. Underfilm creep
Definition: corrosion that advances under intact-looking film from a chip, scratch, or thin edge, often seen after humidity or salt exposure. Buyer impact: units look fine at IQC and fail in the bathroom. Spec tip: if you run salt fog or humidity, define scribe or damage evaluation and maximum creep distance. Link acceptance to the full system (substrate + pretreatment + powder), not powder brand alone. Disposition: usually lot reject for CTQ failures; investigate pretreatment and edge coverage before authorizing rework.
5. Poor adhesion
Definition: film lifts in crosshatch or X-cut tape test below the agreed ASTM D3359 (or ISO 2409) classification. Causes include inadequate cleaning/pretreatment, undercure, contamination, or oil from drawing/welding. Spec tip: state method, tape type if required by the method, locations (flat plate coupon and production wire face), and minimum grade. Disposition: reject; do not ship “maybe OK” adhesion into a wet bathroom program.
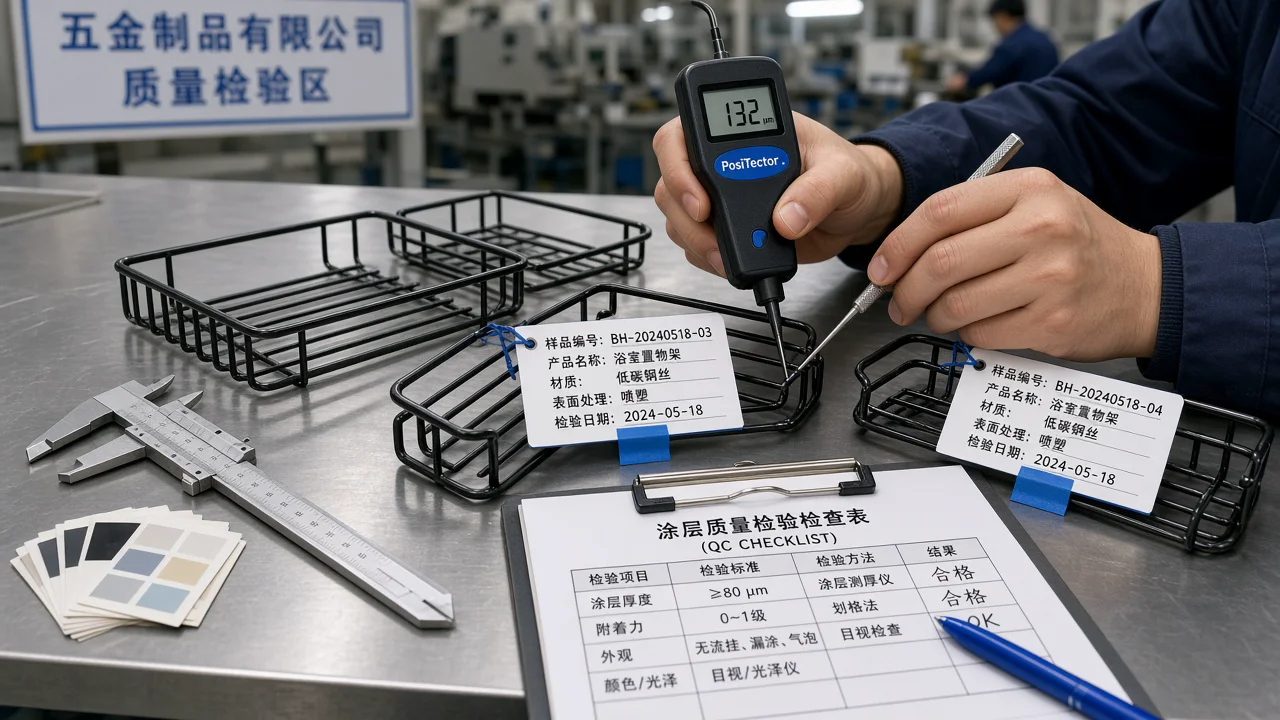
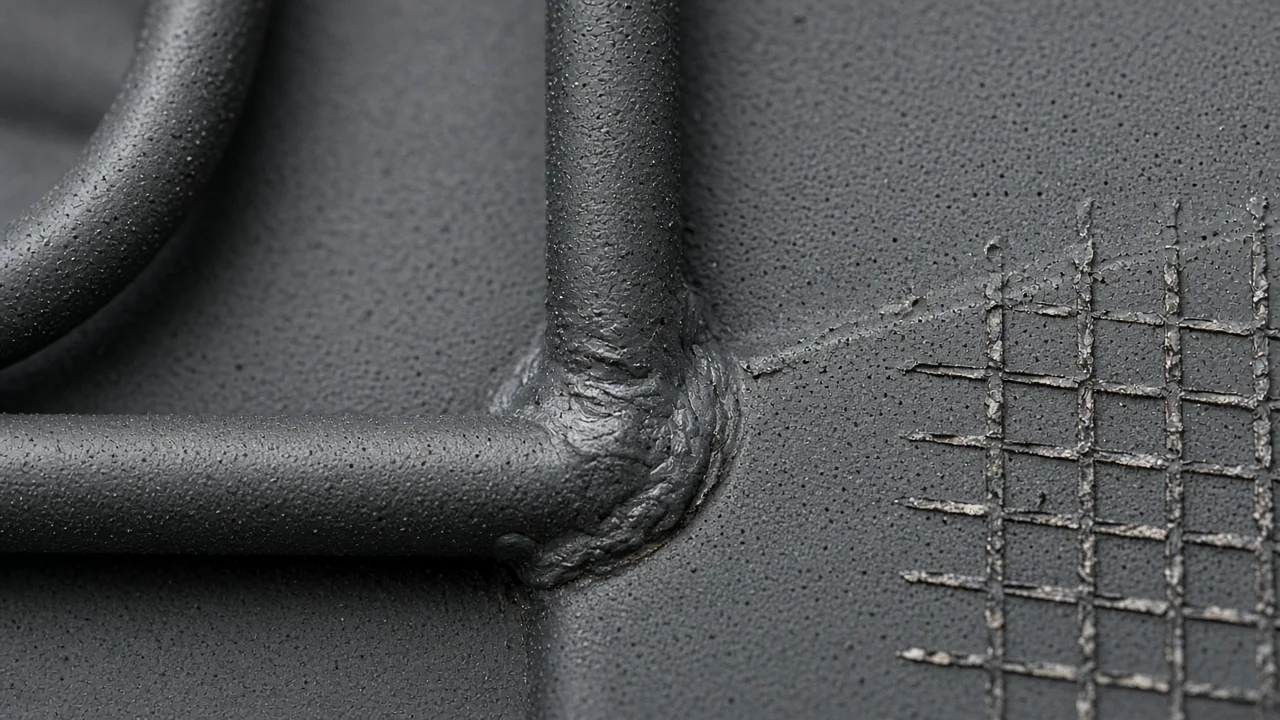
Finally, train both supplier IQC and your inbound auditors on the same accept/rework/reject examples once per season. A fifteen-minute photo review of DEF-03 edge thin film and DEF-10 packaging abrasion prevents most “why did you reject this” emails. Keep the powder coated shower caddy defect catalog beside the weld and dimensional sheets so finish is never treated as an afterthought when the line is late.
FAQ: Powder Coated Shower Caddy Defects and Specs
Is orange peel always a reject?
No. It depends on your photo-spec and brand tier. Heavy orange peel on facing surfaces usually fails retail photography standards; light texture on rear wires may be acceptable if labeled.
Why can flats pass DFT while hooks rust?
Edges naturally pull thinner film. If CTQ edge points are not measured, a powder coated shower caddy can pass paperwork and fail in the shower. Always specify edge locations.
Should every PO require salt spray?
Not always. Salt fog is expensive and ASTM B117 does not by itself define pass/fail for your product. Use it when channel risk justifies representative specimens and clear creep/rating limits. Many programs start with adhesion, DFT edges, and humidity-aware visual/packaging rules.
Can IQC accept liquid touch-up on chips?
Usually no for OEM powder claims in wet zones. Touch-up rarely matches film integrity and often becomes a underfilm creep starter. Prefer reject or controlled strip/recoat.
How many photo masters do we need?
At least one accept and one reject per high-risk defect (edge thin film, pinholes, Faraday corners, packaging abrasion, color). Keep revision control. Update when powder code or texture changes.
Does stainless wire remove the need for coating specs?
No. Many caddies remain coated carbon steel for cost and color. Even coated stainless programs still need adhesion, color, and cosmetic rules. Material choice does not replace defect language.
Where do process controls fit?
Use this defect catalog for acceptance language. Use the humid-bathroom powder coating process pillar for DFT windows, pretreatment, Faraday cage technique, and packaging engineering detail when you audit the line.
How should we label severity on the ten defects?
Start with adhesion fails, bare metal in wet-zone corners, pinholes on wet faces, and underfilm creep as critical or top major. Edge thin film below minimum is usually major trending critical when hooks are the rust starter. Orange peel, mild overcure shift, and non-exposing abrasion are often major or minor by brand. Publish the class next to each DEF ID in the RFQ so AQL switching rules are unambiguous.
What belongs in the first-article pack?
Include labeled photo masters, DFT map, adhesion photos with grade, powder TDS and batch, cure curve, packaging method photos, and a signed defect catalog revision. For a powder coated shower caddy launch, that pack prevents “we never agreed” debates three lots later.
Can we use the same catalog for epoxy and polyester powders?
Yes for defect names. Chemistry differences still matter for humidity durability and overcure behavior, so keep powder chemistry and indoor wet-zone suitability in the finish identity clause. Do not assume an indoor decorative powder will survive condensate because the defect catalog looks complete.
Send Your Powder Coated Shower Caddy Spec for Review
If you are building or revising a powder coated shower caddy program, bring a short brief: target market and wet-zone expectations, wire diameter and weld density, color/texture masters, draft CTQ table (DFT flats/edges, adhesion method and grade, DEF-01–10 photo limits), packaging method, and whether humidity or salt-fog evidence is required. Koitor Hardware supports OEM wire bathroom storage programs from Jiangmen, China, with practical RFQ and IQC language—without pretending one finish recipe fits every SKU.
Share drawings and labeled photo masters via our contact page or email simon@koitorhardware.com. We can help you turn the ten defects above into a supplier-ready acceptance sheet before the next production release.
Recommended attachments: PDF defect catalog with DEF-01–10, two photo masters per high-risk defect, draft CTQ table, and packing method photos. If you already buy from multiple plants, send one failed lot report with unlabeled photos—we can help map them to defect IDs before you renegotiate the supplier quality agreement.
OEM / EIGENE MARKE
Verwandeln Sie diesen Beschaffungsleitfaden in ein Produktdossier
Teilen Sie uns Ihr Zielprodukt, die Größe, die Oberflächenausführung, die Bestellmenge und Ihre Verpackungsanforderungen mit. Ihr Team erhält vor der Angebotserstellung eine praxisorientierte Prüfung der Herstellbarkeit.
 English
 Español
 Português
 Français
 Deutsch
 العربية